Is the tool shake tolerance exceeding the standard when machining super-long boring bar step holes? Damping structure stabilizes boring dimensions
In precision machining production workshops, the use of ultra-long boring bars to process stepped holes often encounters severe tool vibration and drift in dimensional tolerances. This situation is the most fundamental reason why the proportion of product rework remains at a high level for a long time.
At this stage in 2026, most manufacturing companies still rely on simply adjusting machine parameters to force production operations, causing the yield rate index of mass production to be strictly limited to the 76% level for a long time.
Why are step holes always out of tolerance?

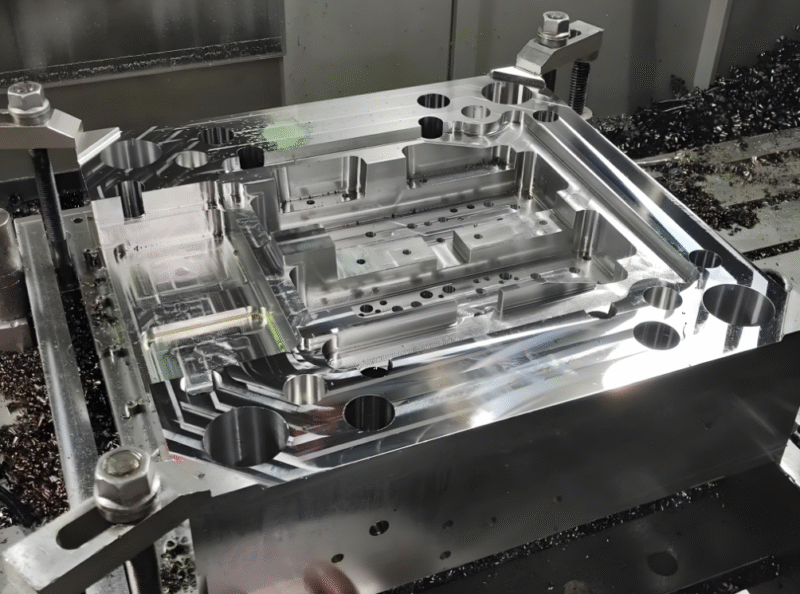
In the hydraulic valve body and mechanical casing, there are a large number of multi-level stepped holes, sink holes and segmented aperture structures. As the hole diameter alternately changes, the cutting load becomes larger and smaller, causing the tool tip to frequently experience forces from one side. Since the rigidity of ordinary extra-long boring bars is relatively poor and there is no vibration-absorbing structure, the result is that the middle section of the rod body begins to deflect and the tool shakes.
The master repeatedly adjusted the speed, feed, and depth of cut, but the jitter during segmented cutting still could not be eliminated. The tolerance of the entire aperture is plus or minus 0.03 millimeters in the fluctuating state. The end face of the step is uneven. Wave-shaped vibration patterns appear on the wall of the hole. The roundness often exceeds the standard range, and the step misalignment often exceeds the standard range.
The real cost of out-of-tolerance
Step holes are core assembly parts. Once the dimensions of multiple sections exceed the tolerance range, there is no way to repair it. The final result can only be that the entire part is directly scrapped. In this way, all resources including material costs and labor hours invested in the previous multiple processing processes are completely wasted. In workshops like the Yangtze River Delta region that focus on precision machining, the scrap cost of a single part due to this reason will generally be higher than the level of three hundred yuan.
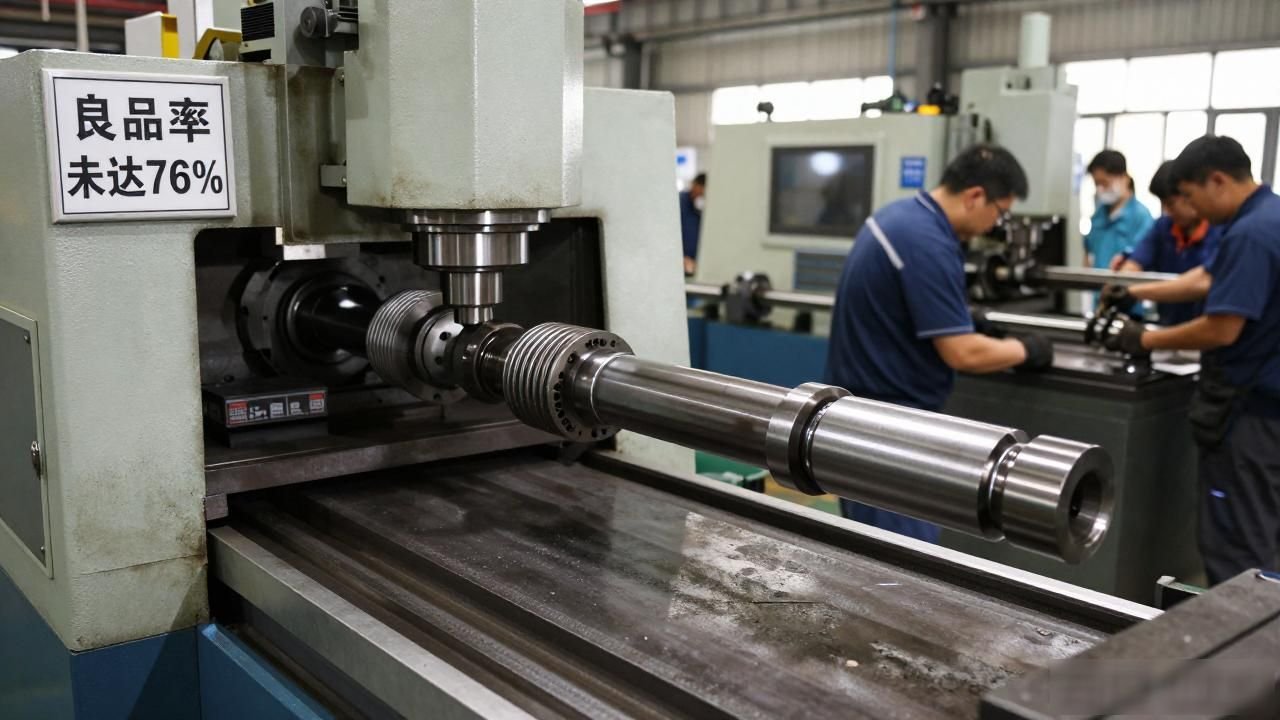
The current batch yield rate has not yet reached 76%. Due to dimensional deviations and end face vibration problems, manual grinding and secondary fine boring can only be relied on, which consumes a lot of machine resources and manpower. Customers complained about lags during assembly, loose seals, and abnormal noises from the equipment, followed by returns and deductions. This behavior directly damaged the factory's reputation.
How does the damping structure suppress the shaking knife?
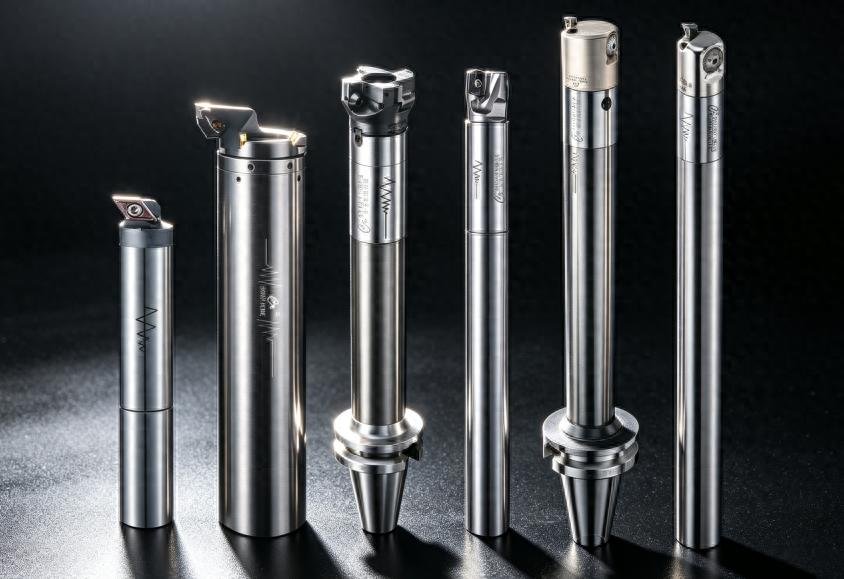
Ruihao damping boring bars are specially designed to cope with the working conditions of step holes, variable hole diameters and intermittent cutting. This kind of boring bar has a passively tuned damping system inside, and is also equipped with a damping weight made of high-specific gravity alloy and a medium that can silently reduce vibration.
These components can quickly absorb the fluctuating vibrations and alternating impacts caused by multi-stage cutting. Through this design, the problem of rod deflection is effectively suppressed. At the same time, the situation of knife tip shaking has also been effectively controlled.
The rod body is forged from high-strength alloy and has undergone multiple heat treatments and ultra-precision grinding during the manufacturing process, so it has very strong rigidity and good resistance to deformation. The runout problem of the end face is strictly controlled to ensure that it is controlled within the range of 0.005 mm.
The tolerance of the entire hole diameter is also strictly limited, lowering it to a level of plus or minus 0.008 mm. This value is nearly four times narrower than the tolerance range allowed by ordinary boring bars.
Comparison of hole wall and end surface finish
After completing the processing of ordinary, super long boring bars, everyone found that very obvious vibration marks appeared on the stepped end face. At the same time, the roughness value of the hole wall surface reaches between 1.6 and 3.2 microns, and the entire surface looks uneven.
Faced with such a situation, each hole must be manually grinded and then subjected to a high-precision secondary boring process. This single production process alone consumes more than half the machine's operating time. With such production efficiency, it is simply impossible to catch up with the batch delivery deadline.
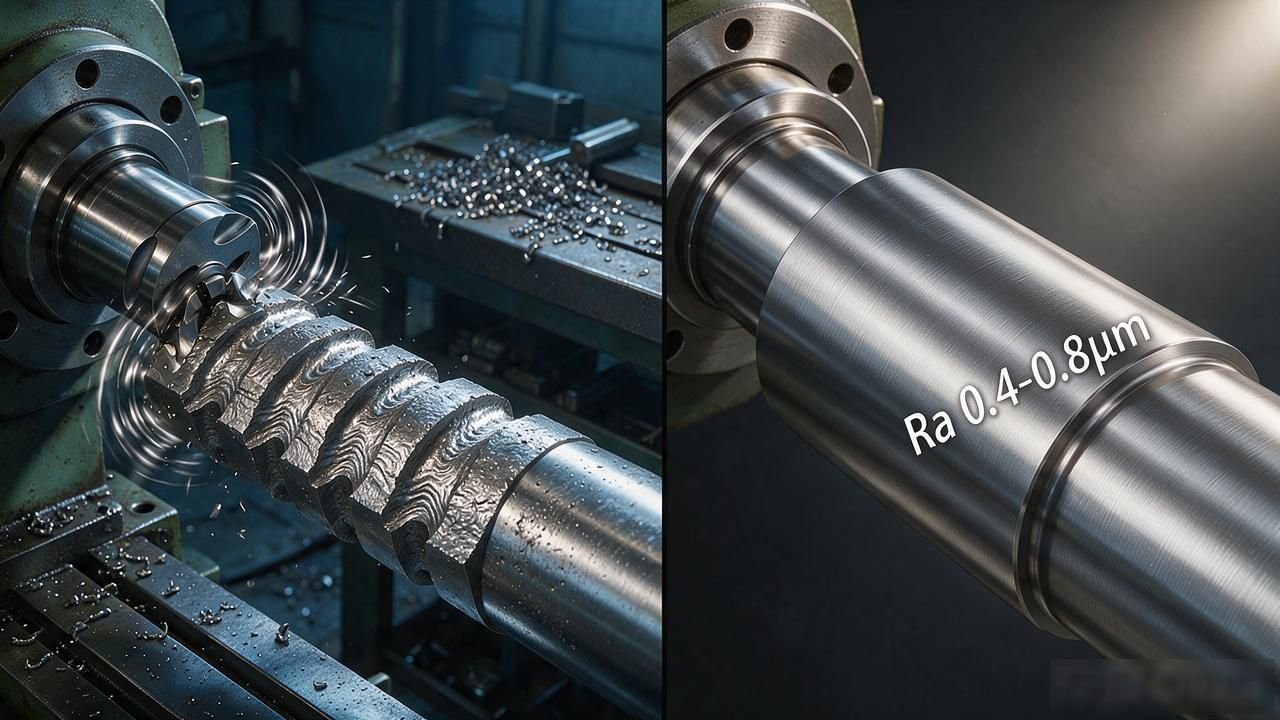
If Ruihao damped boring bars are used, it can be formed in one go without vibration marks or step misalignment. The smoothness can be stabilized in the range of Ra0.4 to 0.8μm, which directly eliminates the grinding process. The quality of the hole wall and end face is clean and smooth visible to the naked eye.
Tool life and machining efficiency
Ordinary boring bars will produce large alternating vibrations and impacts during the working process, which will cause the cutting blade to wear and even chip. The frequency of occurrence is very high, which keeps the tool replacement rate at a high level. The damping structure designed by Ruihao Company can buffer the stress generated during segmented cutting. In this way, the wear of the blade becomes more even during the boring process , and its service life is increased by 65%. The cost of consumables for a single product has also dropped significantly.
In the past, I was forced to lower the parameters for layered slow boring, but now I can directly set the standard cutting parameters. The single-hole processing efficiency has increased by more than 40%, the process yield rate has stabilized at 99%, and the batch production capacity has finally kept up with the pace of orders.
Adaptation range and customization services
This product series is compatible with mainstream machine tool interfaces such as BT, HSK, CAT, etc., and is compatible with various types of precision machining centers and boring and milling equipment. The stock is sufficient. Orders with standard specifications are sent out immediately after the order is placed. The delivery time is relatively short. Is the tool shake tolerance of extra-long boring bar step hole processing exceeding the standard? The damping structure stabilizes the boring size and will not affect the rod changing operation of the production batch.
We support customization of non-standard extra-long overhangs, multi-level apertures and special interfaces. In addition to boring processing , we also provide free machine sample services and provide on-site step hole test cutting support. Our technical team will come to your home to debug the exclusive cutting parameters under variable load conditions, and will provide subsequent after-sales follow-up services for the entire process.
What is the tolerance of step holes in your workshop? Have you ever had the painful experience of being tortured by a shaking knife? Everyone is welcome to chat about this topic in the comment area. If you find the content useful, please like and share it.


暂无评论内容