Introduction to sheet metal laser cutting process
In the sheet metal processing industry, the first mainstream process is laser cutting. However, many masters start to feel headaches once they encounter programming work. As long as there is an error in one parameter setting, the entire batch of materials may be scrapped. In this way, the cost of materials consumed alone may reach thousands of dollars.
Draw the picture first and then talk about cutting
The first step is to draw the outer contour of the part in the CAD software. The key point of this step is that the contour you draw must be closed, even if only a very small corner is broken.
According to the actual usage of domestic mainstream sheet metal factories from 2025 to 2026, they continue to use AutoCAD or SolidWorks to produce drawings. After you finish the drawing, you need to save the file in DXf format.

Converting the file into a DXF format or G-code file that can be read by the laser machine is a very subsequent step. Many people who are just getting started will ignore this step of sheet metal processing laser cutting programming . In this case, the machine will not be able to recognize the image at all, which will make the whole process in vain.
If there are text contents with annotation properties in the image, be sure to delete them, otherwise the cutting equipment will mistake the text for the processing path and perform cutting.
Material size and layout must be determined first
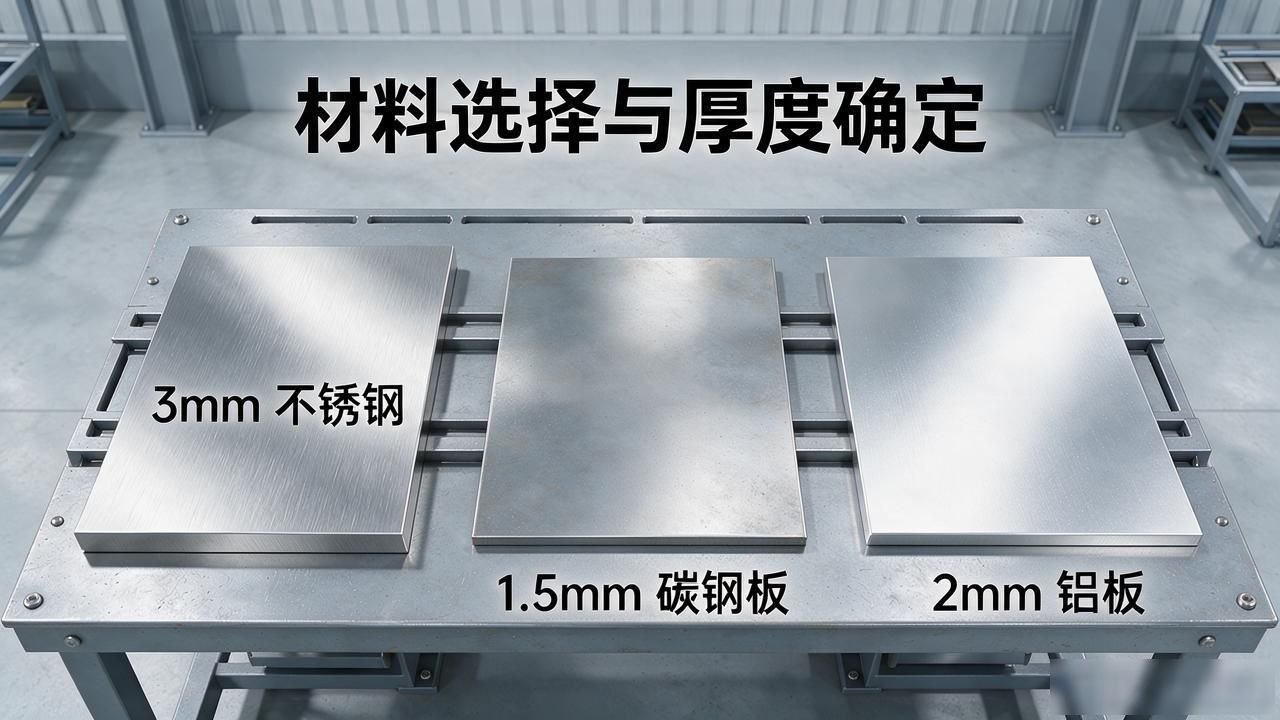
Selecting materials and determining thickness is a very critical prerequisite. What we need to face is that the parameters of 3 mm thick stainless steel, 1.5 mm thick carbon steel plate or 2 mm thick aluminum plate are completely different.
By this time in 2026, 304 stainless steel and SPCC cold-rolled plates are two materials that are often used in sheet metal factories in the Yangtze River Delta region. Before placing an order, you must confirm the inventory situation with the silo.
The layout plan directly determines whether an order is profitable or loss-making. If professional layout software is used for processing, the material utilization rate can reach more than 92%, while relying on manual layout, the utilization rate can only reach about 85%. The difference between the two methods is three to four percentage points. If executed within a long one-month period, the final material cost difference will reach thousands of yuan.
Rounded corners or sharp corners depends on the needs
If the user wants blunt edges, then the rounded corner process should be selected. If the user wants sharp angles, then the loop process should be selected. The chassis shell is generally blunted with rounded corners to prevent sheet metal processing and laser cutting programming , but the sharp corners of the knife mold must be retained. This point only requires one click in the software, but if the selection is reversed, the entire product will have to be scrapped and re-cut.
After selecting the process software, the gas type will be automatically loaded into it. For carbon steel, oxygen is used, and for stainless steel, nitrogen is used. The cutting speed is also automatically matched according to the thickness. Approximately for 3 mm carbon steel the speed is 8 meters per minute. Novices should not manually modify the data randomly. Once it is modified and deviated, the section will become uneven and rough.
Don’t ignore the material return distance
After the laser head has finished cutting a line, it is necessary to lift the knife before it can continue to cut a line. The distance moved by lifting the knife is the so-called return. If this distance is set too short, the laser head will scratch the surface of the workpiece that has been processed and leave an ugly white mark. On the contrary, if it is set too long, the entire production cycle will be lengthened, resulting in a decrease in efficiency, which will cost more than ten minutes or more in processing each batch of orders.
In 2026, most factories will set the withdrawal distance to 1mm to 2mm. When using air-assisted cutting, you must also consider the position of the air blow nozzle, and never block the cutting seam. The parameters are clearly written on the table, so just fill them in according to that. Don't adjust the parameters randomly because you think you can grasp the situation.
Processing sequence affects yield
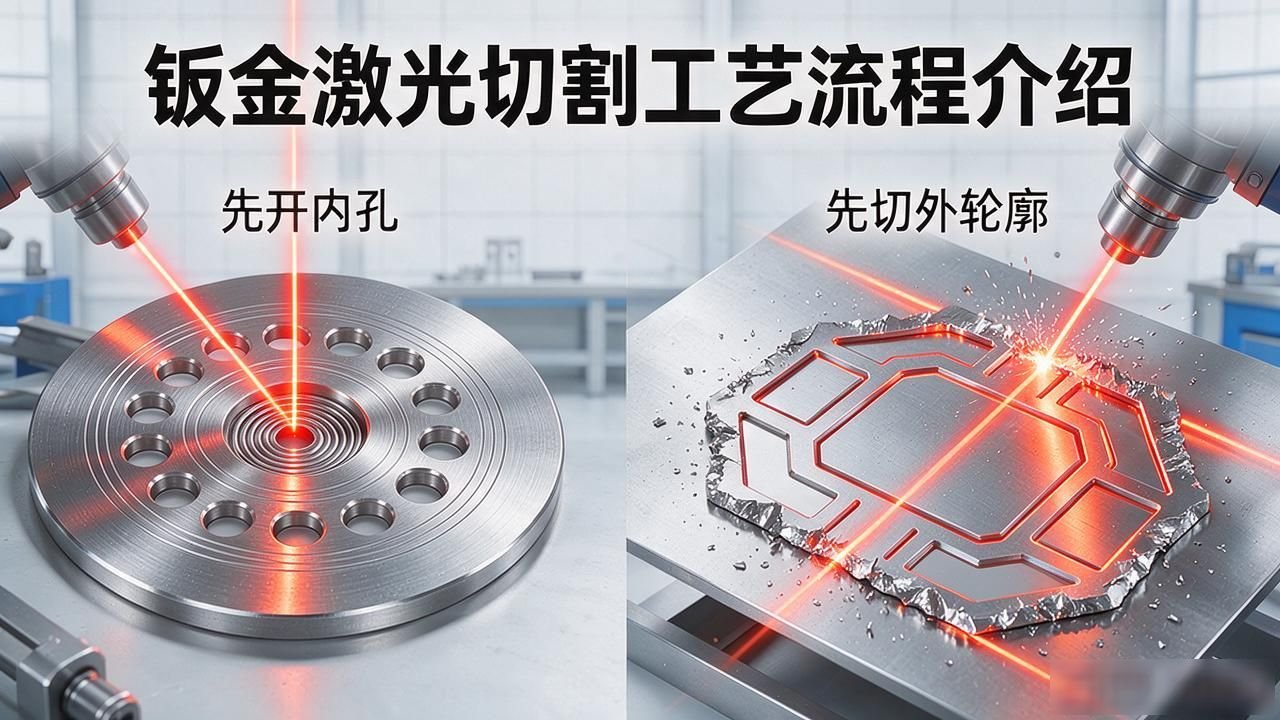
Should you drill the inner hole first, or cut the outer contour first? If the order is reversed, the edge of the part will immediately crack.
Usually everyone has to abide by this rule, which is to cut the small pieces first, and then move to the large pieces. First, deal with the parts that are closely arranged, and then deal with the parts that are relatively sparsely arranged. The starting position of the inner hole should be two millimeters ahead of the outer contour.
In 2024, there was a sheet metal processing factory in East China that reversed the order of this operation, which resulted in a batch of very precisely crafted brackets being turned into scrap products, ultimately causing economic losses of more than 40,000 yuan.
Regarding sequential optimization software algorithms, the maturity level is actually very high now, but for those with rich experience, they are more accustomed to manually fine-tuning some key steps. If the accuracy requirement reaches 0.1 millimeter for parts, even a small amount of deformation will directly lead to a huge gap between failure to pass inspection and final scrap.
Program generation and transfer
After setting all the parameters, click the "Generate Program" button. At this time, the software will output a G-code file or the file content in a device-specific format.
Then transfer these files to the cutting machine controller device through a USB flash drive, a LAN, or a DNC interface. You must know that at a relatively late time point like 2026, large-scale factories will basically use Ethernet direct connection technology to achieve instant and rapid transmission of data.
After the program transfer is completed, perform an empty tool simulation operation to confirm whether the tool paths intersect or a collision will occur. After confirmation, load the material and perform formal cutting. This two-minute simulation session can help you avoid a collision accident, because once the machine's spindle is repaired, it will cost at least several thousand yuan.
When your factory performs laser cutting programming operations, you will introduce the sheet metal laser cutting process. Which software product is used specifically for sheet metal processing laser cutting programming , and then what kind of value can the utilization rate of the layout finally reach? You can communicate and discuss it in the comment area. If you think this content is valuable to you, then please click the like button to express your approval, and forward it to your colleagues in the same industry so that they can also take a look.


暂无评论内容