Automotive body joining technology: welding? Riveting? Who is the best connection solution for body-in-white?
Once the connection process of the body-in-white is chosen incorrectly, it will lead to rework and re-manufacturing in the worst case, and the crash test will not meet the passing standards in the worst case. In 2025, the proportion of most mainstream domestic automobile manufacturers using multi-material car bodies has exceeded 40%.
At this time, the body connection is no longer simply welded, but the most suitable connection method needs to be determined based on the specific parts and different materials used.

Spot welding is the big brother that has been used for fifty years
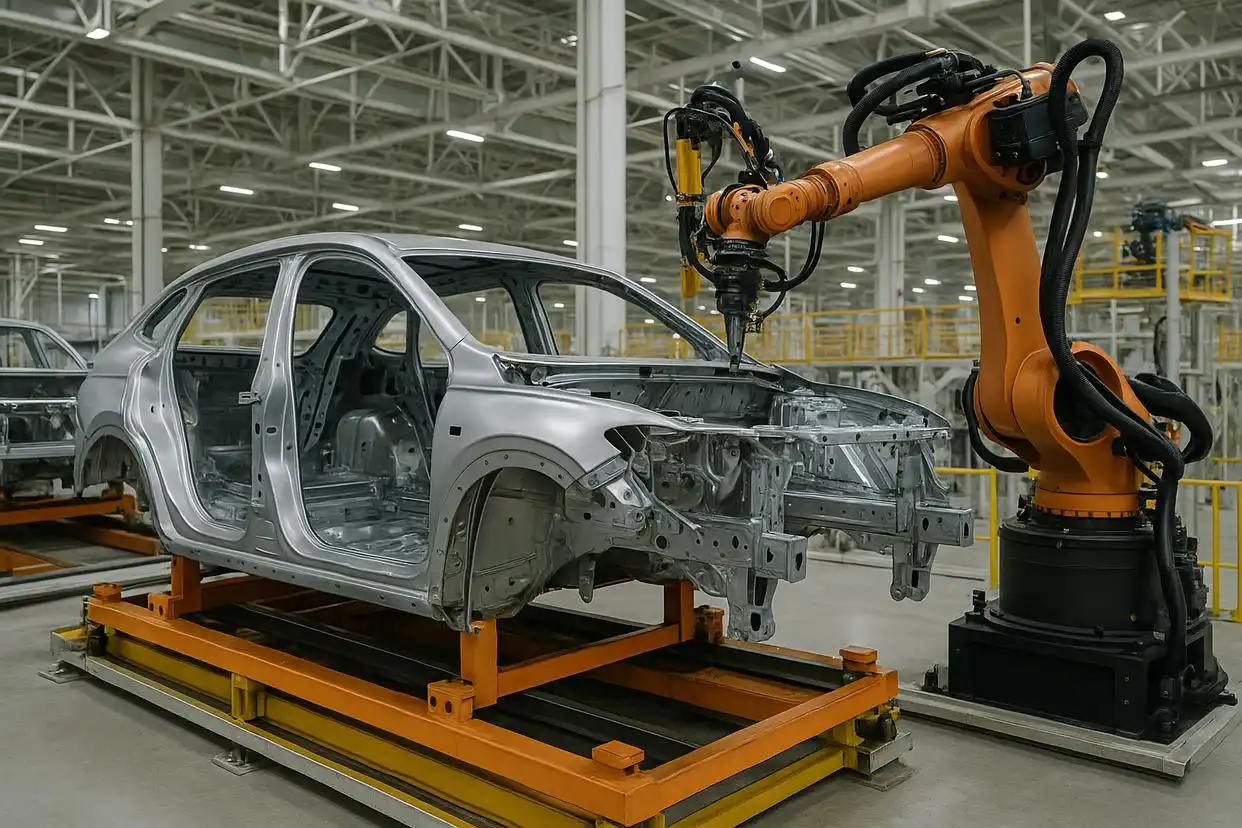
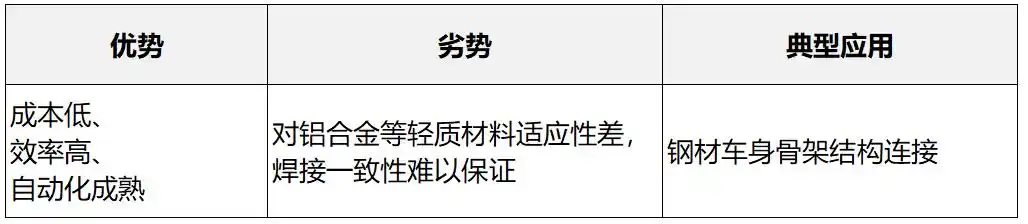
Resistance spot welding still occupies a dominant position in the process of manufacturing steel body-in-white. The average number of welding points contained in a total domestic welding pass is probably within the range of 3,000 to 5,000.
The pressure applied by the welding gun used during welding is within a range of 400 to 800 Newtons. At the same time, the current can reach thousands of amperes, and the two layers of steel plates with a thickness of 0.8 mm can be successfully and firmly welded together in a short period of only two seconds.
<But> This method of spot welding is only suitable for butt welding between steel materials of the same metal. Once it involves aluminum alloy materials or carbon fiber parts, it cannot be used. <In>2024<> in a new SUV model launched by a German brand, after the rear bumper was replaced with aluminum alloy material , the difference between tinplate riveting and bite technology and the selection of automobile body connection technology: welding? Riveting? Who is the best connection solution for body-in-white? , the original number of solder joints was directly reduced by 60%, so the SPR process was used to fill the vacancies.
SPR self-piercing riveting is a new method that does not require pre-holes
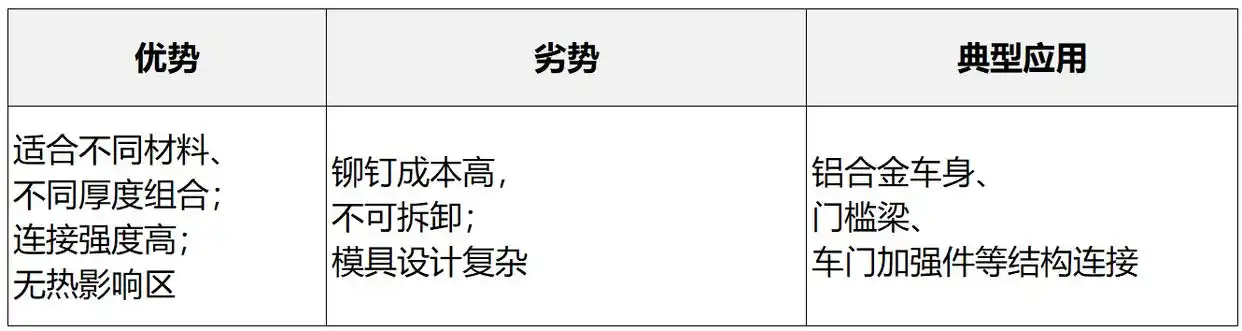
SPR rivets penetrate the upper board from the top. It is then extruded inside the underlying board. In this way, a mutually locked state is formed. The entire process takes less than 1.5 seconds. By 2025, more than 15 domestic OEMs will be involved in the body-in-white process. They launched the SPR station at this stage.
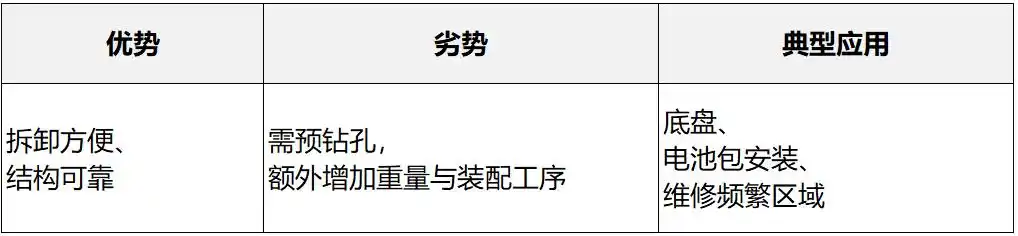
A very big advantage is that it can be connected to steel and aluminum materials, and there is no need to drill the preset holes first.
However, the cost of each rivet point is about three to five times more expensive than traditional solder joints. Automobile manufacturers usually only use it in places where different types of materials are spliced. If it is the connection method of steel to steel, spot welding is still the most cost-effective and cost-effective method.
FDS hot melt screw joint combines hot drilling and tapping in one step
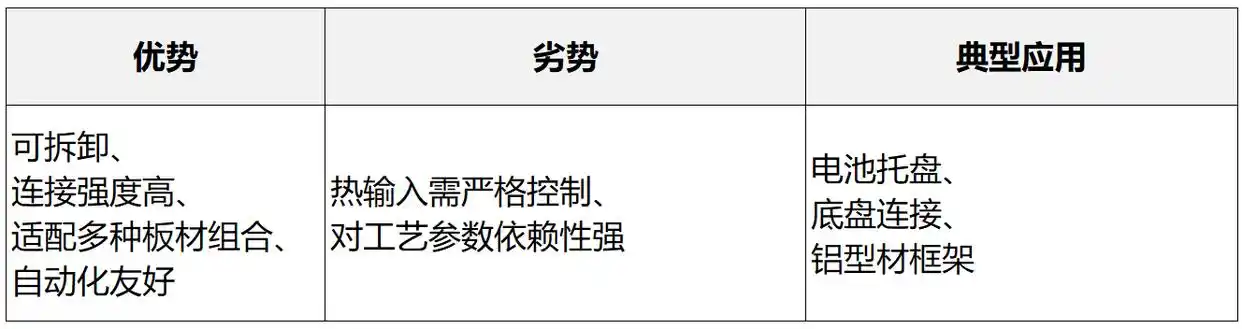
< The FDS drill bit rotates at high speed to generate friction and heat, forming threads while drilling, and then screwing in the bolts to fix it. Adding threads to a hole can be done in 30 seconds. In 2023, a domestic new energy brand's roof beams will use FDS in batches to replace traditional screw connections.
The bicycle method saves 12 pre-drilling processes, so the cycle time becomes much faster. However, since FDS technology has an upper limit on the thickness of the plate, once it exceeds 3 mm, it cannot be drilled, so at this time, it is necessary to switch to plasma cutting and then perform tapping operations.
Biting and gluing are old partners in sheet metal sealing
The so-called bite process is actually to take two boards, fold them and interlock them together and then tap them tightly. This situation is common in white iron air ducts and small sheet metal parts of the car body. Among them, the depth of the bite is generally eight to fifteen millimeters. It relies on mechanical interlocking to bear force, so it does not rely on connection methods such as welding points or rivets.
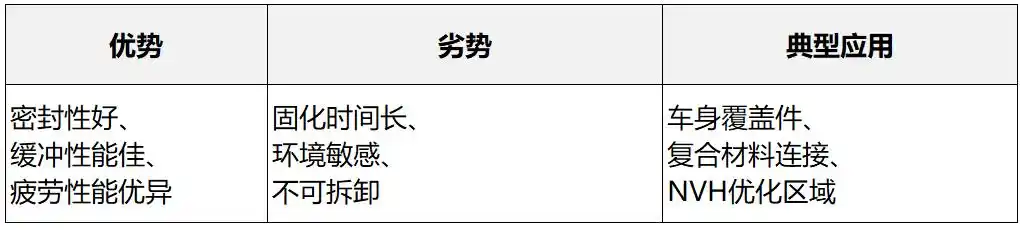
The so-called glue application is to apply structural glue on the surface that needs to be overlapped, and then perform a pressing operation to solidify it. Normally, as long as the thickness of the adhesive layer reaches the range of 1 to 2 mm, it is enough to withstand the requirements of the shear force.
According to the current situation of the industry, by 2025, whether it is glass installation work or door anti-collision beam fixing work, it will basically rely entirely on the technical method of gluing. By applying in this way, the installation process of hundreds of bolts can be saved.
Choose different techniques for different parts, don’t mix things up
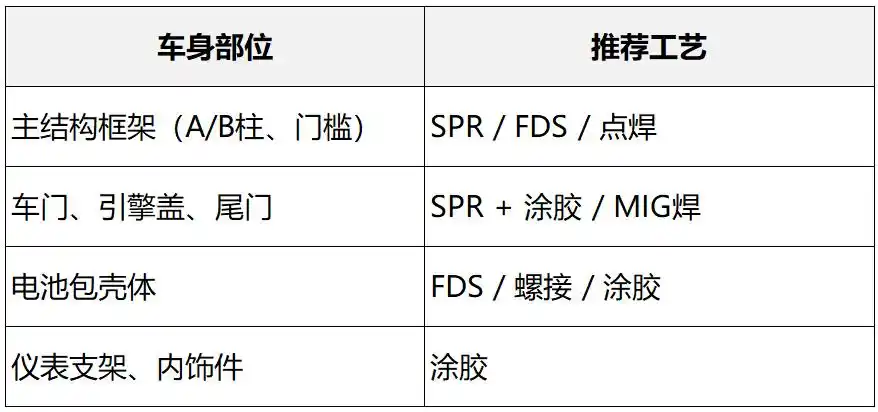
For frame parts such as the A-pillar and B-pillar that are used to withstand force, the connection between steel and steel still uses a combination of spot welding and adhesive coating to form a double protection measure; the aluminum alloy beams on the roof are connected using SPR; the thinner plates inside the engine compartment are fixed using FDS technology and bolts. Each component is arranged in an orderly manner according to its location and material characteristics, and each is in the appropriate position.
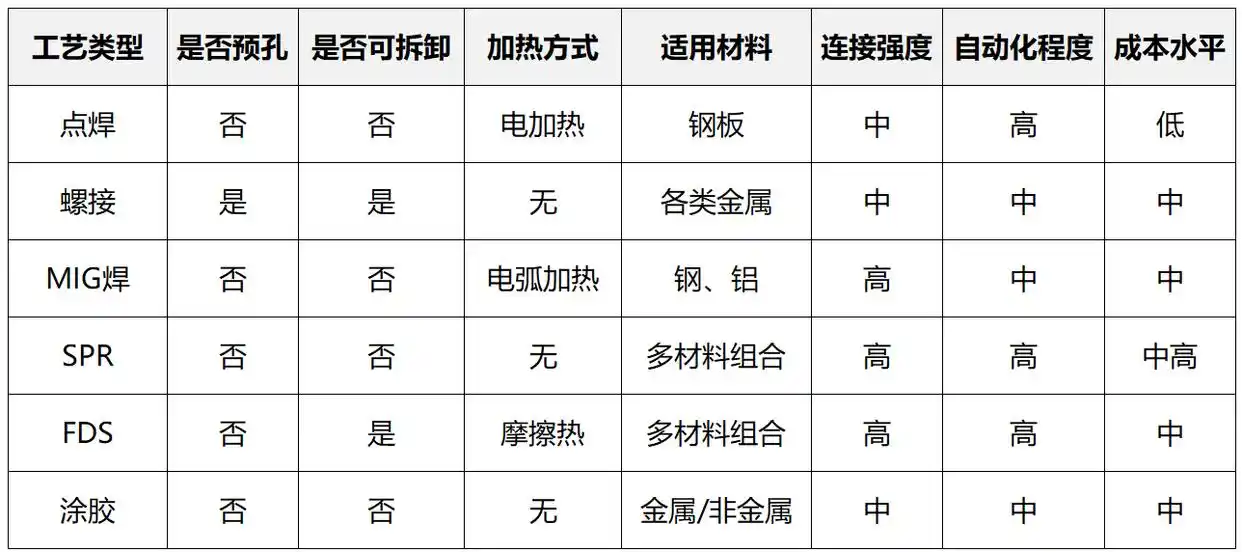
For collision safety parts that require detachable repairs, priority should be given to bolting and gluing. For those structural splicing scenarios that cannot be disassembled, the use of self-piercing riveting technology will be more stable and reliable.
The 2024 version of the national standard GB has put forward new technical requirements in terms of crash performance, which has formed more stringent regulations on the stiffness indicators of the car body. Currently, many manufacturing plants have replaced their original spot welding processes with self-piercing riveting processes. After this conversion, the body stiffness data increased by 8%.
There is no optimal, only the right
By 2026, the method of connecting the body is already a combination of spot welding, SPR to supplement the position, FDS to improve efficiency, and glue for sealing. There is no single process that can cover all parts.
When choosing a process, you need to put the four aspects of materials, cycle time, cost, and maintainability on the table for comparison and measurement. Don't just focus on who has better welding strength. May I ask what level the proportion of steel-aluminum hybrid parts in your production line has reached?
Is it because the spot welding method can no longer withstand the current production pressure, or the cost of SPR has not been effectively reduced? Welcome to share your opinions and experiences in the comment area. If you think this content is useful, click like and forward it to colleagues in the workshop.




暂无评论内容