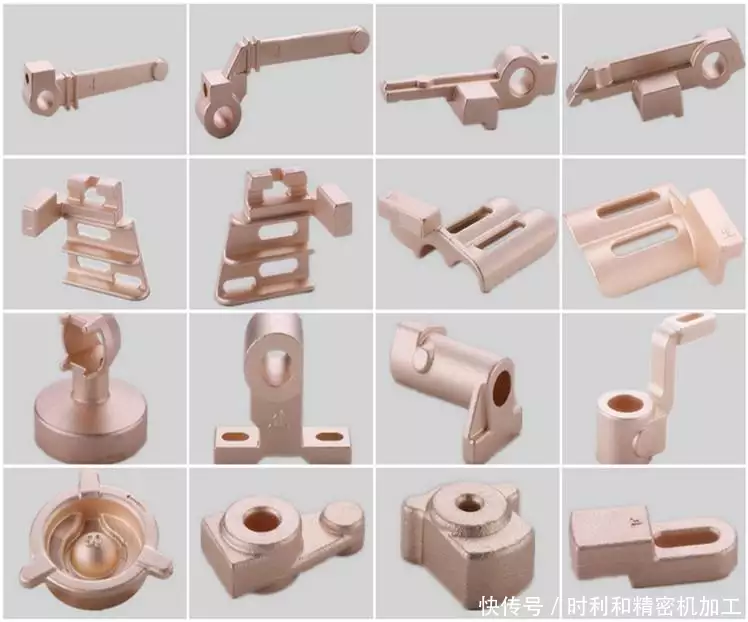
Non-standard metal parts processing: strict testing, worry-free quality!
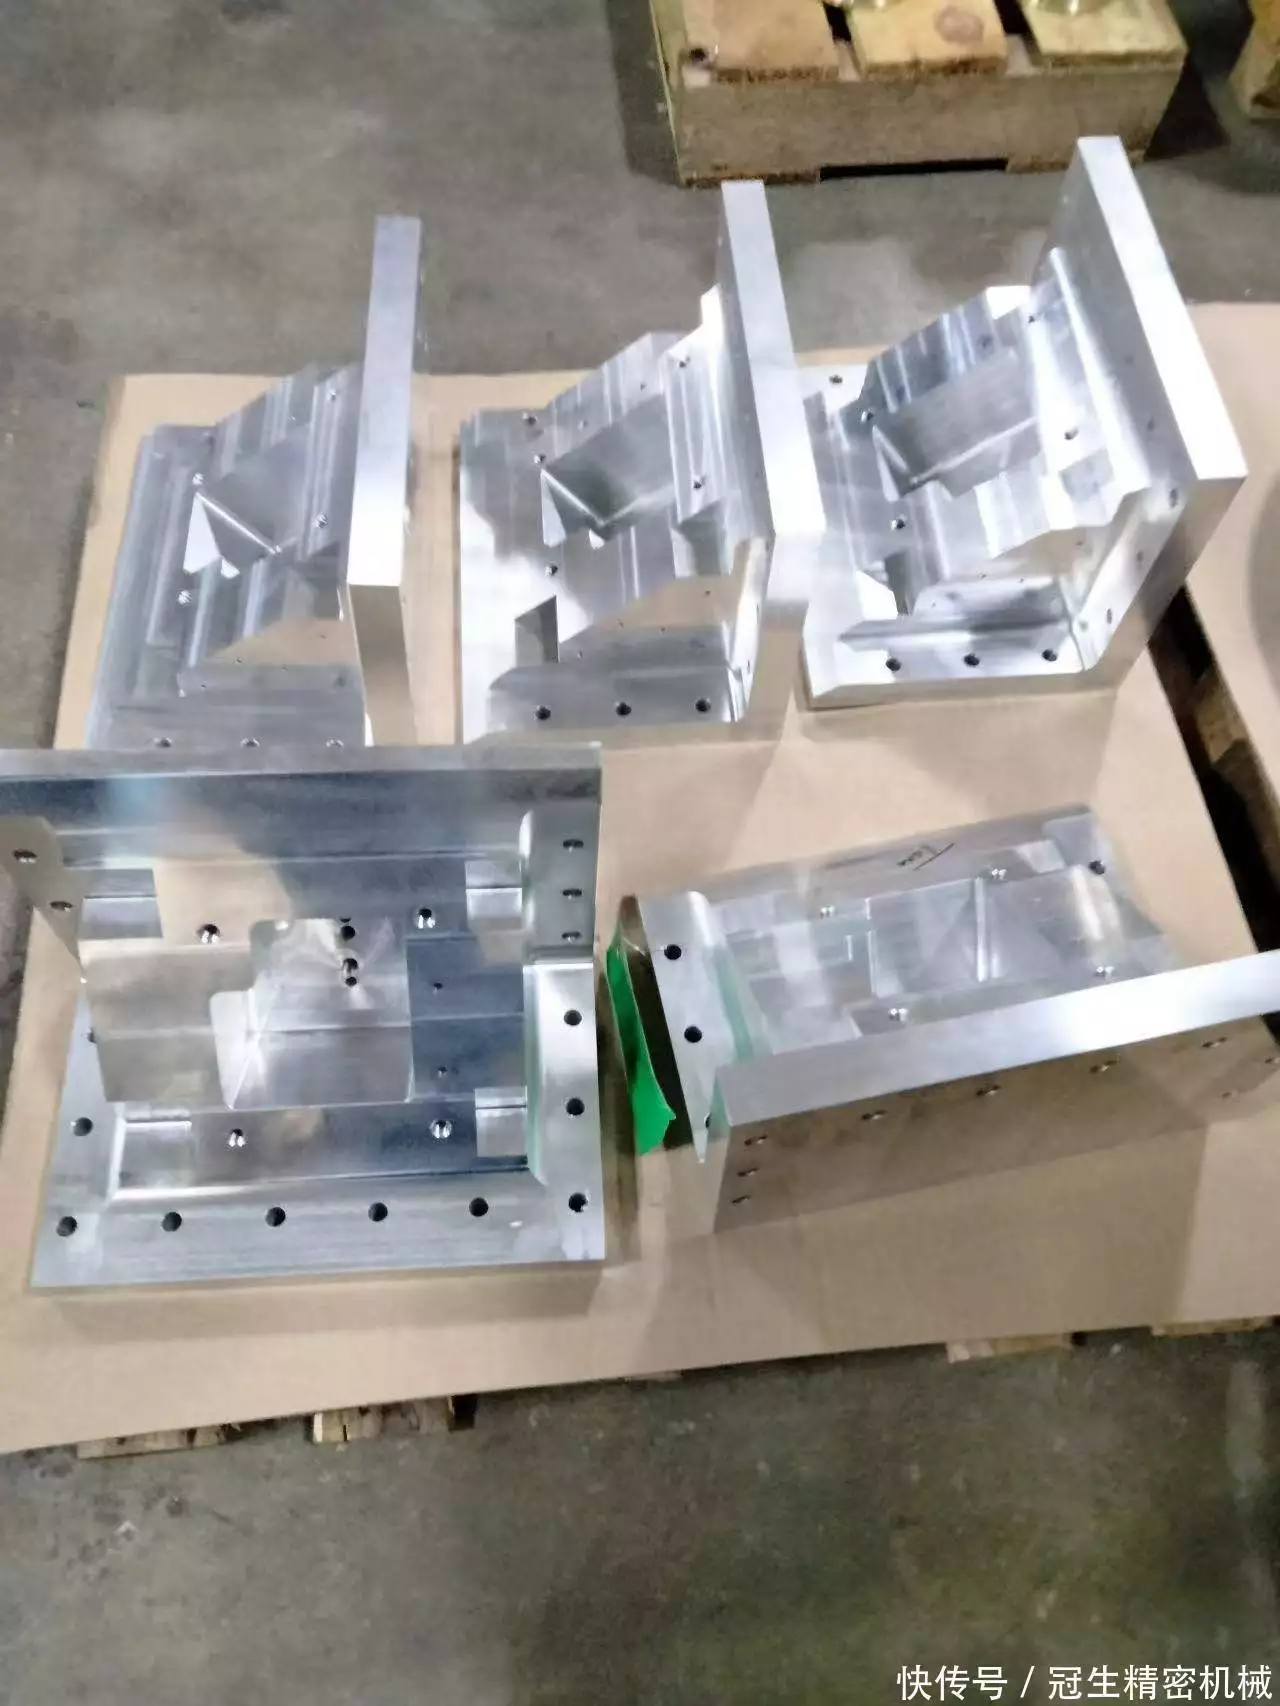
When dealing with non-standardized metal parts, even a small deviation of 0.02 millimeters may completely scrap the entire equipment. At this stage in 2026, the specific accuracy requirements for precision instruments and industrial equipment are still developing in a more extreme direction. Therefore, whether the inspection system at the processing plant is effective or not can directly determine whether the customer dares to give the order to you.
Raw materials entering the factory first pass through the spectrometer.
Stainless steel, aluminum alloy and titanium alloy are three different materials, and their corresponding standards are completely different. In 2026, a factory that manufactures precision instruments put forward clear requirements. The nickel content of 304 stainless steel must be maintained at no less than 8%, and the hardness of the aluminum alloy must exceed HRC30.
When raw materials enter the factory, the first step is to send them to a spectrum analyzer for testing. Once the chemical composition is found to be substandard, they will be returned directly for processing, and those blanks with cracks or deformations will be rejected.
Don't underestimate this step. Although it is time-consuming, if you bring poor quality materials into the workshop, all the subsequent cutting and drilling work will be in vain.
According to statistics from some machining parks in 2025, rework due to problems with the material accounts for more than 40% of all quality-related accidents. Therefore, checking the quality from the beginning is the most cost-effective way to save money.
After cutting and drilling, three coordinates must be passed

Because the key process has just ended, the parts are immediately sent to the three-dimensional coordinate measuring machine and laser caliper for processing. Regarding the problem of hole diameter and shaft diameter deviation, it needs to be strictly controlled within the range of plus or minus zero point and one millimeter.
At the same time, the specific conditions of geometric tolerances such as parallelism, perpendicularity, etc. must also be verified one by one. If the relevant data does not meet the specified standards, the processing parameters need to be adjusted immediately. This is another approach that must not be adopted, that is, you cannot save a batch of products first and then review and judge them collectively.
There is a factory in Jiangsu that specializes in non-standardized parts. At the beginning of 2026, online real-time testing was launched. Then the proportion of unqualified batches dropped from 2.3% to 0.4%. In this month alone, it saved almost 150,000 yuan in rework costs. Dynamic testing is definitely not a superfluous approach. It is the only way to truly achieve that accuracy.
Surface quality cannot be judged by sight alone
After the product is manufactured, a roughness meter needs to be used to scan and inspect each surface to identify existing scratches, burrs, oxide scale and other problems one by one.
If it is for customers who produce outdoor equipment, additional tests on corrosion resistance and pressure resistance must be added to simulate those harsh operating conditions. You know, as long as the surface roughness is slightly lower than half a grade of the standard, the service life of the seal will be directly cut by half.
In 2025, something happened at a manufacturer that provided industrial equipment in the southwest region of Shandong. Because the burrs on the surface of the parts were not cleaned very thoroughly, the equipment had leakage problems after the parts were assembled.
This resulted in a batch of equipment requiring repair work. The repair work was delayed for a full three weeks. It can be seen that the core competitiveness of non-standard parts processing enterprises cannot be saved in the process of surface inspection.
Simulation assembly is the last gate before leaving the factory
The parts themselves do not exist in isolation. Only by rotating them together with the supporting parts can problems be discovered. Before the product officially leaves the factory, these parts must be put into a simulated assembly scene for actual operation to detect their fit, running clearance, tightness, etc.
All the testing data must be saved and archived in the end, and a report can be traced. In this way, customers can directly check the relevant data by scanning the QR code.
By 2026, more customers will choose to include the statement "test reports must be provided with the goods" into the contract terms. For those processing plants that cannot even provide complete inspection records, even if your quotation is very low, you will never get an order. This is because customers simply do not dare to bet on all the losses caused by the sudden stop of the equipment.
Inspection capability is the strongest sign of a processing plant
Nowadays, people in the same industry are competing fiercely for the total number of equipment and delivery dates. What can really make a significant difference is the construction of the inspection system.
The specific performance is from the spectrum analysis link, to the measurement using a three-dimensional coordinate measuring machine, and then to the implementation of simulated assembly actions. The data in this entire continuous process can be traced forward. This state directly leads to a significant reduction in the cost that customers need to spend to establish a trust relationship. At the same time, the customer's subjective willingness to cooperate has been significantly improved.
A company engaged in the processing of non-standard parts successfully obtained the certification of the ISO 10012 measurement system in 2025. As a result, the renewal rate of large customers suddenly increased from 68% to 91%. This illustrates a very clear fact. The testing system that cannot be more perfect is definitely not a cost center that only spends money, but a core and important tool that can help companies acquire customers.
The money saved by testing is far greater than the equipment investment
The price of a three-dimensional coordinate measuring machine is hundreds of thousands, but as long as one part is scrapped, it is very likely to cause losses to the customer, such as the entire production line having to undergo a debugging cycle. If analyzed from the perspective of the general ledger, the cost of inspection is actually only a fraction of the loss caused by rework. The core competitiveness of non-standard parts processing companies is to allow those qualified parts to directly enter the assembly process. In this way, This can save delays caused by equipment debugging and costs incurred in secondary processing.
The processing must be precise, and the testing must be very strict, so that there is no worry about quality. These twelve words may seem simple, but when implemented on the ground, it turns into six sets of equipment and a complete set of processes. This is because what customers want is not the lowest price at all, but a sense of certainty that they can use it directly after handing over the thing.
How many steps of testing did those non-standard parts in your factory actually undergo before leaving the factory? You are welcome to come to the comment area to tell us how you did it. If you think this method is useful, then please like the core competitiveness of non-standard parts processing enterprises and forward it to your peers for a look.


No comments yet