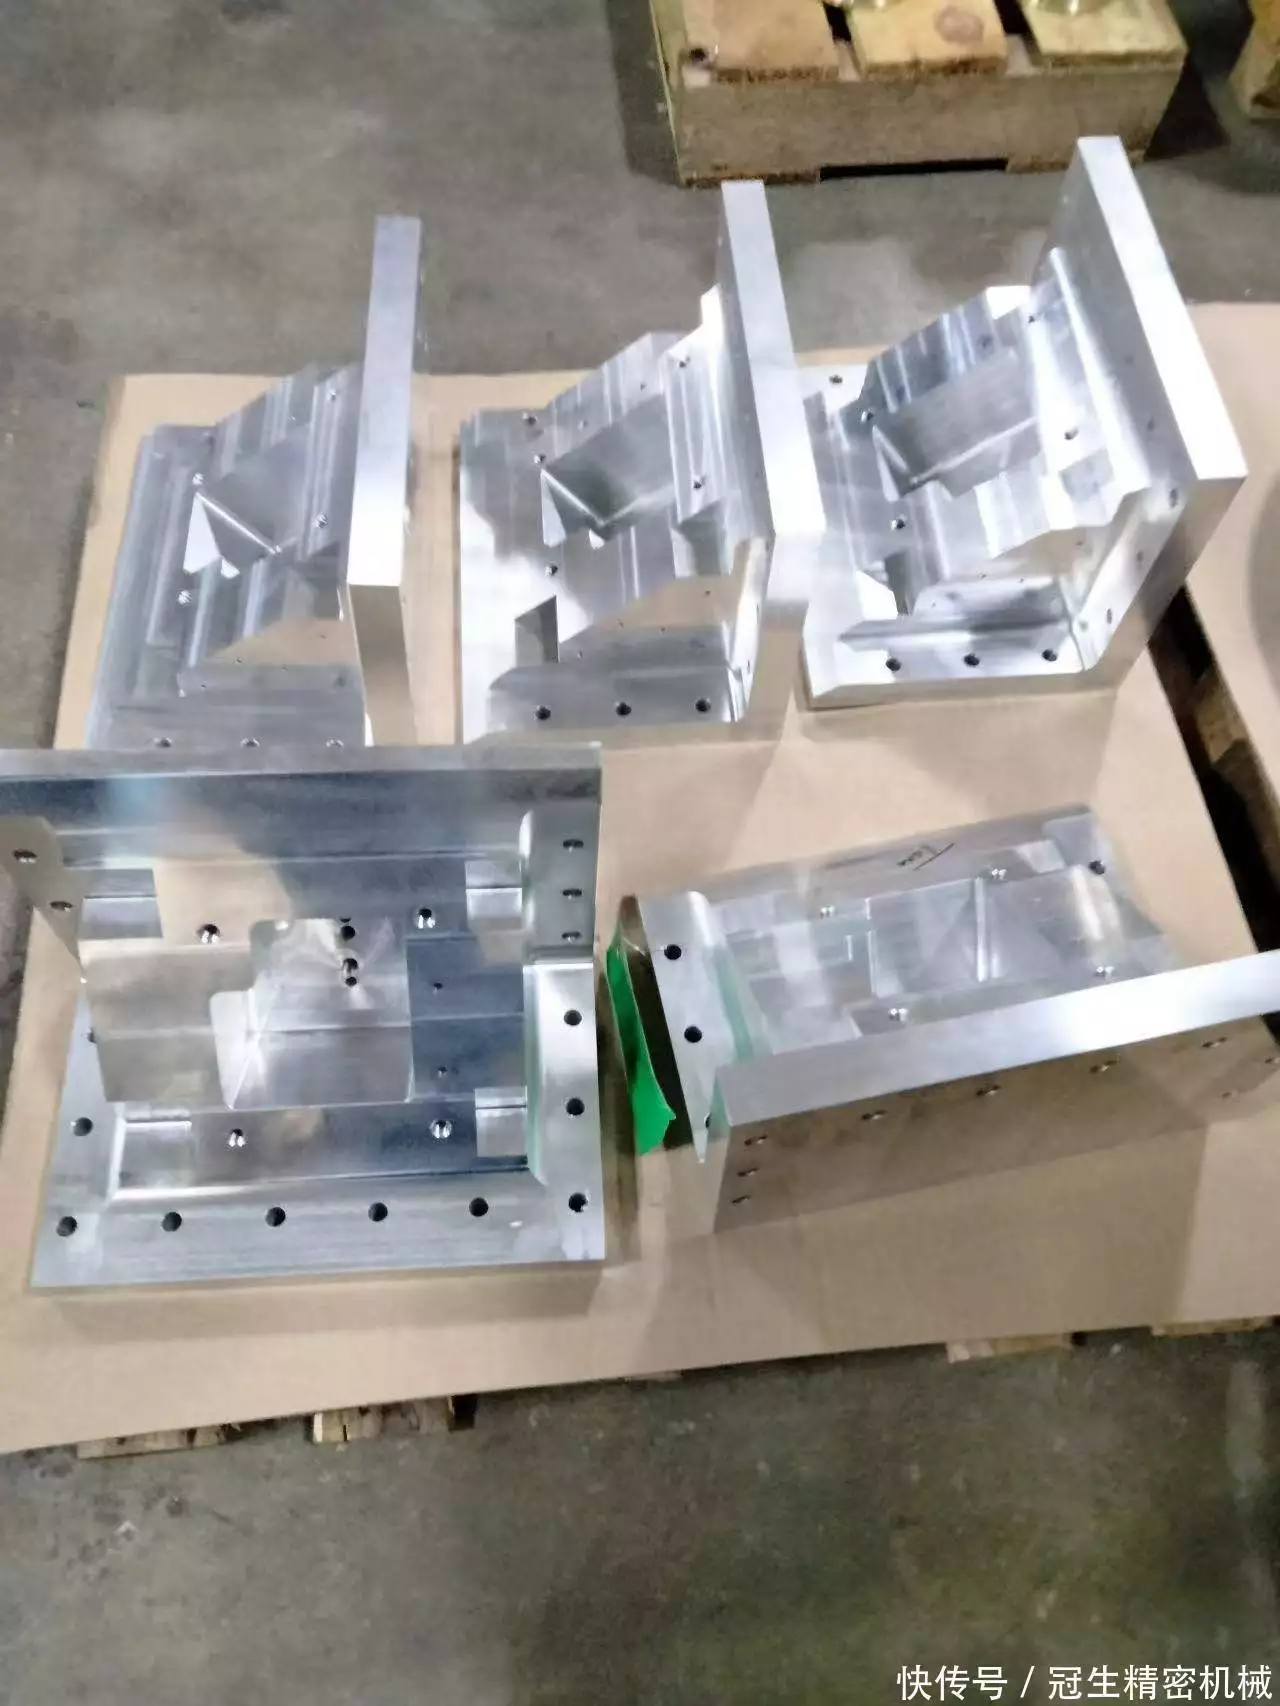
Cast iron welding flat plate cast iron welding platform riveting welding flat plate for sale > HD pictures
The agricultural machinery casing made of cast iron is very hard and also quite fragile. If you are not careful during riveting and welding operations, the weld seam will crack. Many people have failed because of this. The main reason for their failure is that they fell on the welding plate. Specifically, they chose the wrong size or placed it in the wrong direction. In this way, the entire work was in vain.
You can’t just put a flat cast iron plate on it
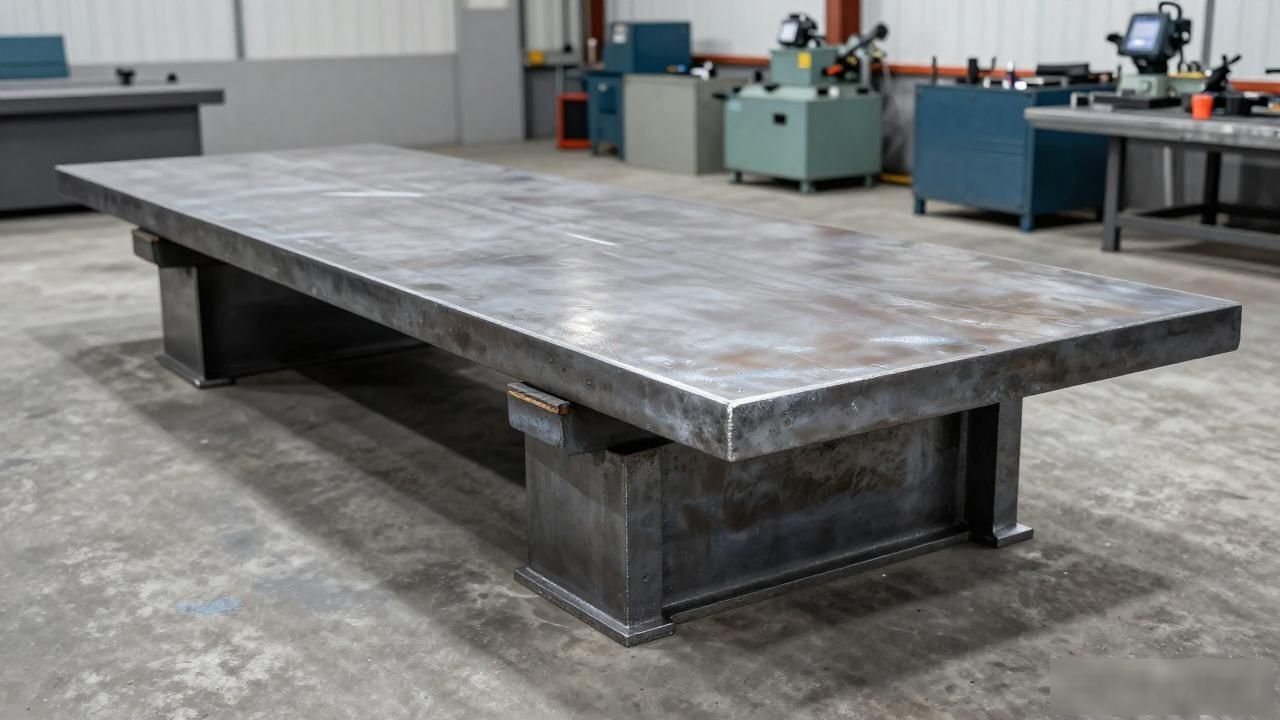
When riveting and welding agricultural machinery casings, the flatness of the flat plate must be controlled within a range of no more than 0.02 mm per meter. The material used is usually HT250 gray cast iron, and its hardness must not be lower than HRC30.
During the production process, several old factories located in Xingwan Town, Hebei Province usually set the thickness of the flat plate to between one-third and one-half of the maximum side length of the shell. If the flat plate is made too thin, deformation will occur.
The area of the flat panel must be larger than the projected area of the casing, and the larger part must be at least 150 mm in size, so that necessary operating space can be left around. In 2024, a factory in Cangzhou that produced agricultural machinery accessories reported this situation to them.
Previously, they used a thin board to cushion the work, but as soon as the shell was placed on it, it would warp, and the rivet holes were all offset by two millimeters. In the end, everyone had to go back to work three times to get this thing done.
Before riveting and welding, measure the dimensions of the shell.
The wall thickness of the casing of agricultural machinery is usually set in the range of 3 mm to 8 mm, and the diameter of the rivets is selected according to the ratio of three-eighths of the wall thickness. Specifically, when using a plate with a thickness of 8 mm, it should be equipped with rivets with a diameter of 3 mm.

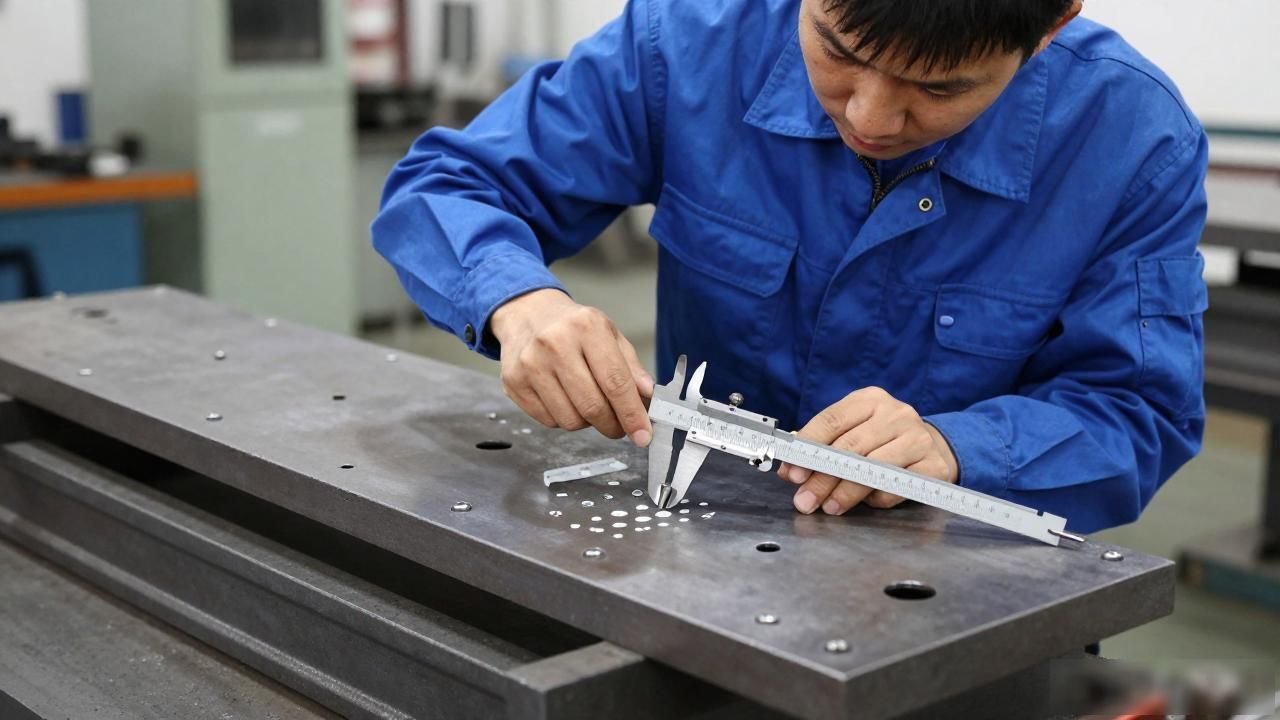
Before installing and connecting the upper plate and related components, a measuring tool such as a caliper must be used to clearly mark the position of each rivet hole and the exact starting and ending points of the weld, and these marked points must be aligned and checked one by one with the positioning holes on the upper plate. You must not rely on visual estimation to complete this alignment work.
In 2025, Lao Zhang from an agricultural machinery repair shop in Luoyang said this. When he was operating in the past, he always placed the housing components based on his feel. Because cast iron parts become slippery when heated, parts that are riveted often become misaligned, with the amount of displacement being between three and four millimeters.
Later, he welded two special positioning blocks on the flat plate. Just put the shell there and it will be firmly stuck in place. As a result, the proportion of rework dropped significantly from 20% to less than 10%.
The order of riveting first and then welding cannot be reversed.
The standard method for cast iron casings is to first punch through all the rivet positions, then rivet them tightly, and then run the weld along the seams. If you just weld first and then rivet instead, the cast iron will expand when heated and the rivets will be squeezed loose. After cooling, the shell will bulge, causing all the rivets to become weak.
When welding, you must be on the flat plate, starting from the middle position and moving to both sides alternately. You must not push the road to the end all at once.
An agricultural machinery manufacturer in Hebei Province has already stipulated the rules in the 2025 process card, requiring that the length of a single weld bead must not exceed 200 mm, and then pause for about three seconds in the middle to allow the accumulated heat to dissipate before continuing to weld the next segment.
Cast iron deforms more when heated than carbon steel
HT250 cast iron is a material with slow thermal conductivity and poor toughness. After welding and cooling, all the residual stress will be held on both sides of the weld, which will cause both ends of the shell to tilt downward and the rivets to loosen. Carbon steel is a material that can be broken back, but cast iron cannot be broken off. How to rivet weld an agricultural machinery casing made of cast iron. How to rivet weld an agricultural machinery casing made of cast iron. How to rivet weld an agricultural machinery casing made of cast iron. Cast iron welding flat plate. Cast iron welding platform. Riveting welding flat plate. > High-definition pictures, it will crack directly.
Therefore, when using a flat plate for work, it is necessary to place two square steel pieces of equal height at the bottom of the casing. The purpose is to prevent the entire bottom surface from being directly attached. In 2025, an agricultural machinery factory in Weifang, Shandong Province conducted a data test on this method. The results showed that after the operation of padding the square steel, the amount of warpage of the casing was reduced from the original 1.2 mm to a range of less than 0.3 mm. And complaints about loose rivets are almost non-existent.
There is a big difference between whether the flat surface is polished or not.
When a newly produced cast iron flat plate leaves the factory, its surface roughness usually reaches the standard of Ra1.6. However, when the bottom surface of the shell is placed on it, a situation will occur, that is, it will be directly chewed into the groove-like pit, which will lead to a 0.5 mm deviation in positioning. After the surface roughness is reduced to Ra0.8 after polishing, the shells can be closely fitted together, so that the position of the rivet holes will be accurate. The starting and ending points of the weld will not deviate.
However, do not use a whetstone for fine grinding, because the debris generated during the grinding process of cast iron will adhere to the installation surface. When the welding operation is performed, the high temperature of the arc will burn the debris into the molten pool, causing the formed weld to be full of pore defects. A senior craftsman in a workplace in the Xingwan area made a statement in 2024, pointing out that it is enough to use fine sandpaper with a mesh of one thousandth of an inch and one eight hundredth and gently tap it once for processing. Never over-sand.
After the work is done, the slab must be rust-proof
The cast iron flat plate is the least afraid of being affected by moisture, especially during the rainy season in the south. If it is placed directly on the ground, a layer of floating rust will form on its surface after one night. Therefore, after completing the work, you need to wipe the surface with a dry cloth and evenly apply a thin layer of machine oil. Then place it on a dry shelf. At the same time, the shelf must be kept at least 200 mm away from the ground and do not allow it to directly contact the wall.
Every time you use it, you must use a feeler gauge to check the flatness. If you find that any piece has been hit, or is worn a little off, and the flatness error exceeds the standard of 0.03 mm per meter, you need to find a mechanic to re-scrape it.
Several tablet manufacturing factories in Xingwan will provide repair services, but if you bump into a pothole during operation, you will have to bear the cost of repair.
When your factory produces cast iron casings and implements riveting and welding processes, what type of flat plate does it use? How is the size determined? Everyone is welcome to communicate and discuss in the comment area. If you think this content is helpful to you, please like it and forward it to your friends for reference.


暂无评论内容