Is the deep hole boring tool pattern of the automobile valve body uneven? The processing smoothness of Ruihao's anti-vibration boring bar reaches the standard
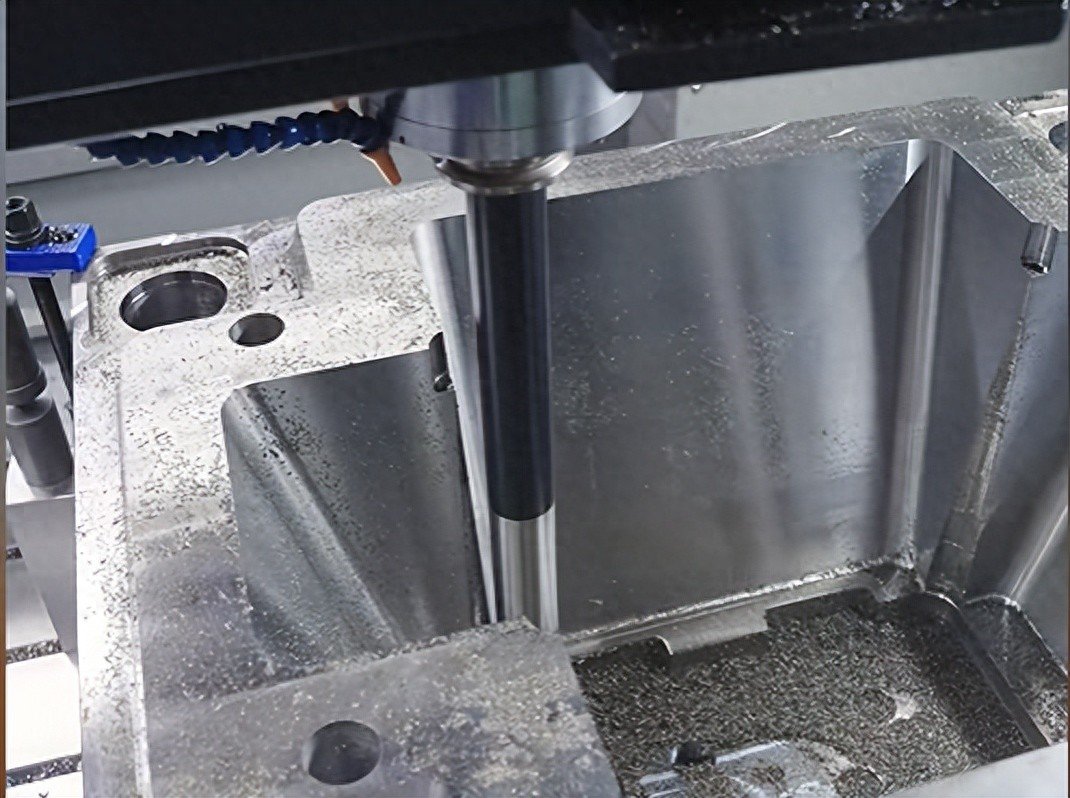
Nowadays, many people are performing deep hole boring processing of automobile valve bodies. When using machine tools, the overhang length is usually between eight and twelve diameters. As soon as it is turned on and operated, it is prone to jitter. This results in spiral patterns all over the hole walls. There are also uneven knife marks. Because of these problems, rework and scrap rates in factories have remained high.
Why are deep holes in the valve body prone to vibration?

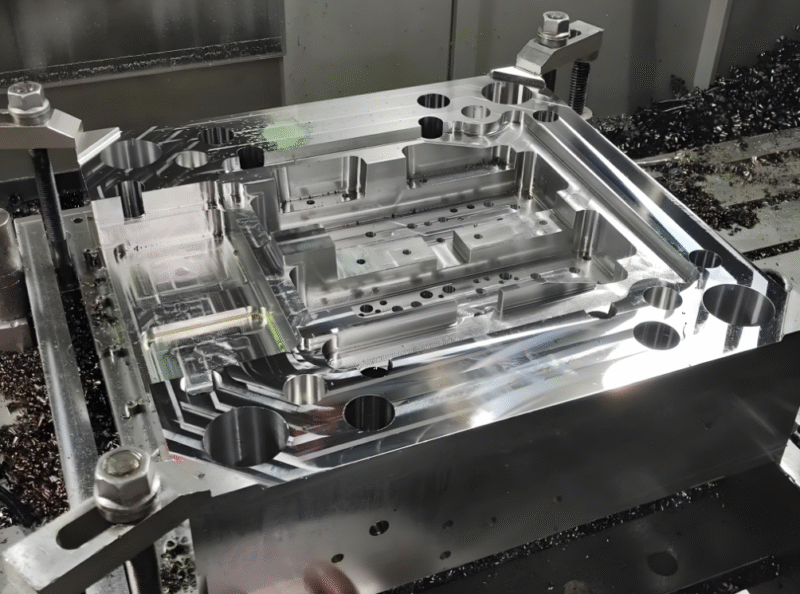
The deep hole in the oil circuit in the valve body has a very small diameter, but a very large depth. The length of the boring bar that extends out can often be as long as eight to twelve times the diameter. Ordinary extended boring bars are not rigid enough. There is a slight jump in the tip of the knife, which will be directly engraved on the inner wall of the hole. No matter how the speed and feed volume are adjusted, the high-frequency resonance phenomenon cannot be suppressed.
Many manufacturers of hydraulic valve bodies in Dongguan and Changzhou have said that if the texture is uneven, the valve core will become stuck or the hydraulic oil will leak. Moreover, this kind of problem always occurs frequently. It has become a common thing for customers to spot check and then return the valve and charge a deduction.
The true cost of not using the knife pattern
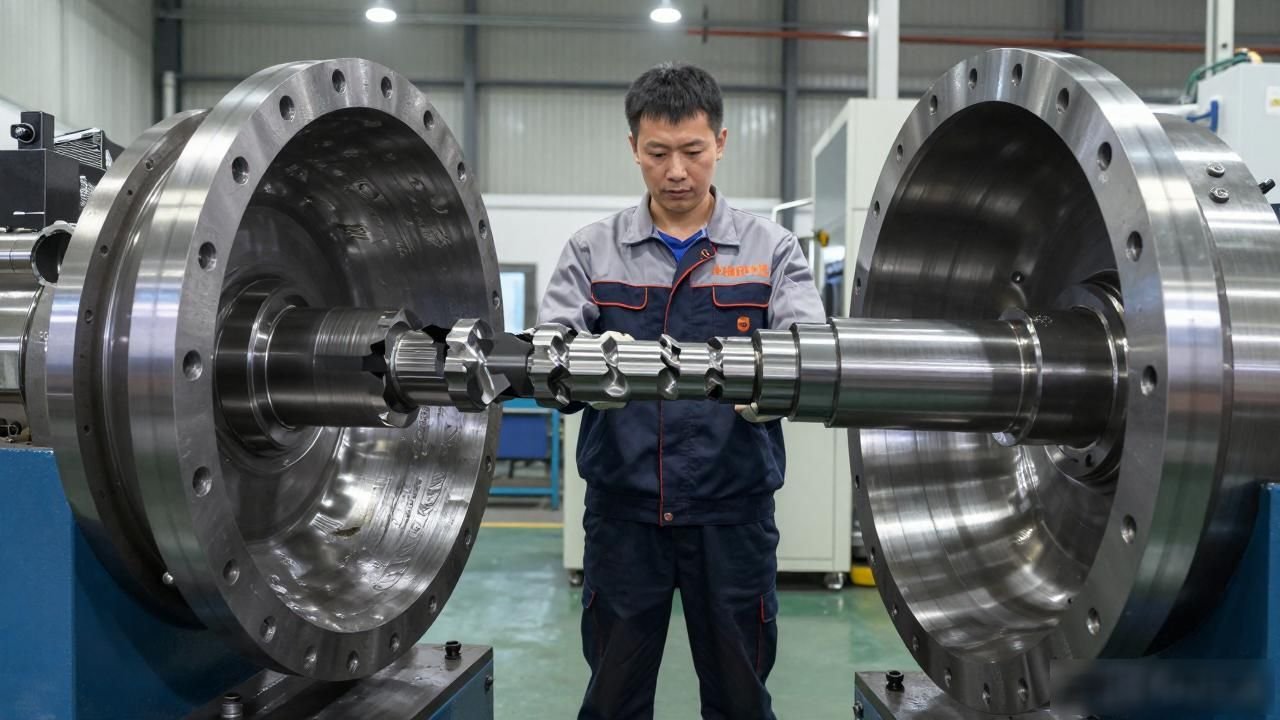
For those lines in deep holes, they must be processed through manual honing and polishing. Each hole takes at least half an hour to grind. If any part is scrapped, the loss can often reach thousands of dollars. The operator therefore has no choice but to reduce the processing speed and use shallow cuts. In this way, the processing cycle of a single hole will be extended to ninety minutes.
The product yield rate has been stuck below 70%. Approximately seven to eight blades need to be replaced every day. The use time of consumables and processing man-hours add up, resulting in the delivery time of bulk orders having to be extended even longer again. Therefore, the supply qualification is at risk of being downgraded.
How to suppress vibration of damped boring bars from the root
The inside of this specialized boring bar produced by Ruihao is boring. Boring processing. Boring processing . Deep hole boring of automobile valve body. Is the tool pattern uneven? Ruihao's anti-vibration boring bar has a machining finish that meets the standard. It is equipped with a passive tuned damping structure. This structure uses an alloy with a particularly high specific gravity as the counterweight material, and is also filled with media to reduce sound and vibration. In this way, the resonance phenomenon caused by the long suspended part of the tool can be quickly absorbed, so that the front end of the tool will no longer have the problem of micro-jumping.
The rod body is made of high-strength alloy and has been forged. It also undergoes multiple heat treatment operations and is then cryogenically shaped. The end face runout will be controlled within 0.005 mm, which can adapt to the interfaces of mainstream machine tools such as BT, HSK, and CAT.
Computer data comparison is clear at a glance
The surface roughness range of ordinary boring bars is between 1.6 and 3.2, and the roundness deviation value is plus or minus 0.03. When switching to the Ruihao boring bar for one-time machining, the surface roughness can reach 0.4 to 0.8, and the tolerance is strictly controlled at plus or minus 0.008. No ripples are visible on the hole wall, and there is no wire drawing.
The processing time was shortened from ninety minutes to fifty minutes, the life of the blade was increased by as much as 60%, and the yield rate of the entire process was directly raised to the level of 99%. As a result, a large chunk of the cost of each single hole was cut off.
How to arrange factory samples
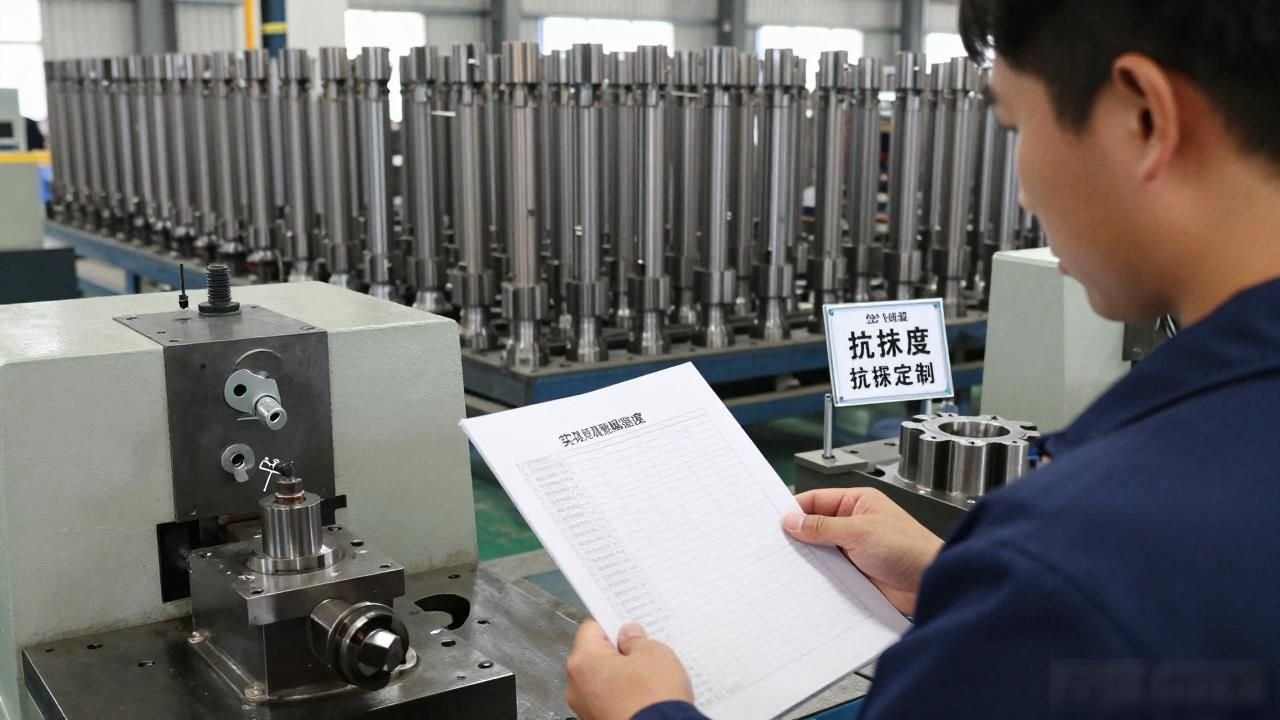
Ruihao has its own factory in Dongguan. The stock inventory is very sufficient, and it supports services such as non-standard overhangs and special aperture customization. It can also provide on-site trial cutting services for the valve body. As for the specific performance, the operator will explain it with the measured roughness report.
The technical team will come to your door to debug the parameters in person. They will come up with an exclusive plan based on the material of your valve body and the depth of the hole. They will follow you throughout the entire process from the first sample to mass production and launch, so you don't have to figure it out on your own.
How to guarantee mass production, quality and delivery
After the deep hole finish reaches the stable standard, the sliding accuracy and hydraulic sealing performance of the valve core are no longer affected by the residual knife pattern factor. When the customer found out that the product passed the test once during a random inspection, the return deduction was basically at zero.
Forcibly reducing the number of scraps per piece to a very small ratio of one percent, this frees up the number of products produced and shortens the delivery time for batch orders from the original three weeks to more than ten days. The qualification certification for supply becomes stable.
Now when the valve body in your factory undergoes deep hole processing, at what value can the surface roughness be stably controlled? Please talk about the specific situation in the comment area. If you find these contents useful, please like and forward them to your workshop director.



暂无评论内容