Inventory of the basic usage steps and maintenance measures of precision CNC cylindrical grinders
Cylindrical grinding is a processing technology, and its processing accuracy level directly determines the service life of bearings and the reliability of aviation components. However, there are many production workshops due to insufficient standardization of operations. This will cause the roundness of the ground workpieces to exceed the standard range, and the surface roughness will not meet the specified requirements. The final result is that the entire batch of workpieces will be discarded. Therefore, the entire process of precision CNC cylindrical grinding machines from startup to later maintenance will be described in detail.
Environment and grinding wheel inspection before start-up
Before starting the machine, be sure to confirm that the temperature in the workshop is stable to the cylindrical grinding accuracy level , and that the temperature value is within the range of 20±1°C. At the same time, make sure that there are no things like stamping machines and cranes around the machine tool, because these equipment are sources of vibration.
Next, check the condition of the lubricating oil tank, the hydraulic station, and the coolant tank to see if the liquid levels in these three places are within the range indicated by the scale lines. Finally, check the workbench and guide rails to make sure there are no residual iron filings generated from the previous batch of production.
It is necessary to focus on checking whether there are cracks on the grinding wheel, and also check whether the balance label is within the validity period. If the time exceeds the specified balancing period or there is a bump on the surface of the grinding wheel, then the static balancing operation and the dynamic balancing operation must be performed again. If this is not done, radial runout will occur during high-speed rotation, eventually causing the roundness index to directly exceed the allowable error range.
Workpiece clamping and grinding wheel selection
For shaft workpieces, the center and tailstock are used for clamping operations, while when dealing with short sets of parts, a hydraulic chuck should be used. After the installation is completed, the coaxiality inspection needs to be carried out, and the error must be controlled within the range of less than or equal to 0.005 mm.
Regarding the selection of grinding wheel material, it needs to be determined based on the hardness of the workpiece itself. When facing a hard workpiece that has been quenched, CBN material or diamond material should be selected. If it is an ordinary steel workpiece, white corundum is suitable as the material. As for the particle size, the range of P80 to P120 can usually be used.
After installing the grinding wheel, you need to use a flange to tighten it. The degree of tightness must be moderate. After all installations are completed, a high-speed idle balancing operation should be performed. Only when the measured runout is less than 0.01 mm, the subsequent program processing is allowed. If this necessary step is omitted, then in the subsequent work process, the overall accuracy will definitely not be effectively guaranteed.
CNC parameters and processing procedures

When operating the CNC system, you first need to set the origin of the workpiece coordinate system, and then enter the grinding allowance, feed speed and grinding wheel linear speed. This program usually includes four cycles of rough grinding, fine grinding, smooth grinding and dressing. Specifically, in the rough grinding stage, a margin of 0.05 to 0.1mm will be left, while in the fine grinding stage, a smaller margin of 0.01 to 0.02mm will be left.
Now that an online measuring instrument is equipped, the first task is to calibrate the probe and make sure that the measured readings are completely consistent with the values on the standard gauge block.
After the program file is officially imported into the system, the paper tape simulation function should be used for verification. Only after it is confirmed that the tool trajectory has not deviated, the instruction data package can be downloaded to the equipment for execution. This is intended to fundamentally and effectively avoid the risk of tool collision accidents caused by errors.
Trial run and first article inspection
The coolant system must be started first, and then a low-speed idle stroke operation must be performed to check whether the distance between the grinding wheel and the workpiece is appropriate and whether the dresser is operating normally. After the first piece is ground, use a micrometer to measure the size, use a roundness meter to detect roundness, and use a roughness meter to measure the Ra value. Only after confirming that all indicators are qualified can the mass production process be started.
Record the data of the first piece in the quality report. The report should include roundness, runout, surface roughness Ra and dimensional deviation. If it is found that the roundness value has changed by more than 0.5μm or the surface roughness Ra value is a little larger than 0.4μm, then first check the trimming interval and feed parameters. Never adjust the machine tool carelessly.
Formal processing and process monitoring
After the automatic cycle is started, the equipment will complete all processing steps in sequence. The operator needs to be nearby and listen to the sounds made during grinding. Under normal circumstances , the cylindrical grinding processing accuracy level is a uniform and fine rustling sound. Once there is squealing or the sound suddenly quiets down, it means that the grinding wheel has been dulled or the workpiece is slipping. At this time, the operator needs to press the emergency stop button immediately.
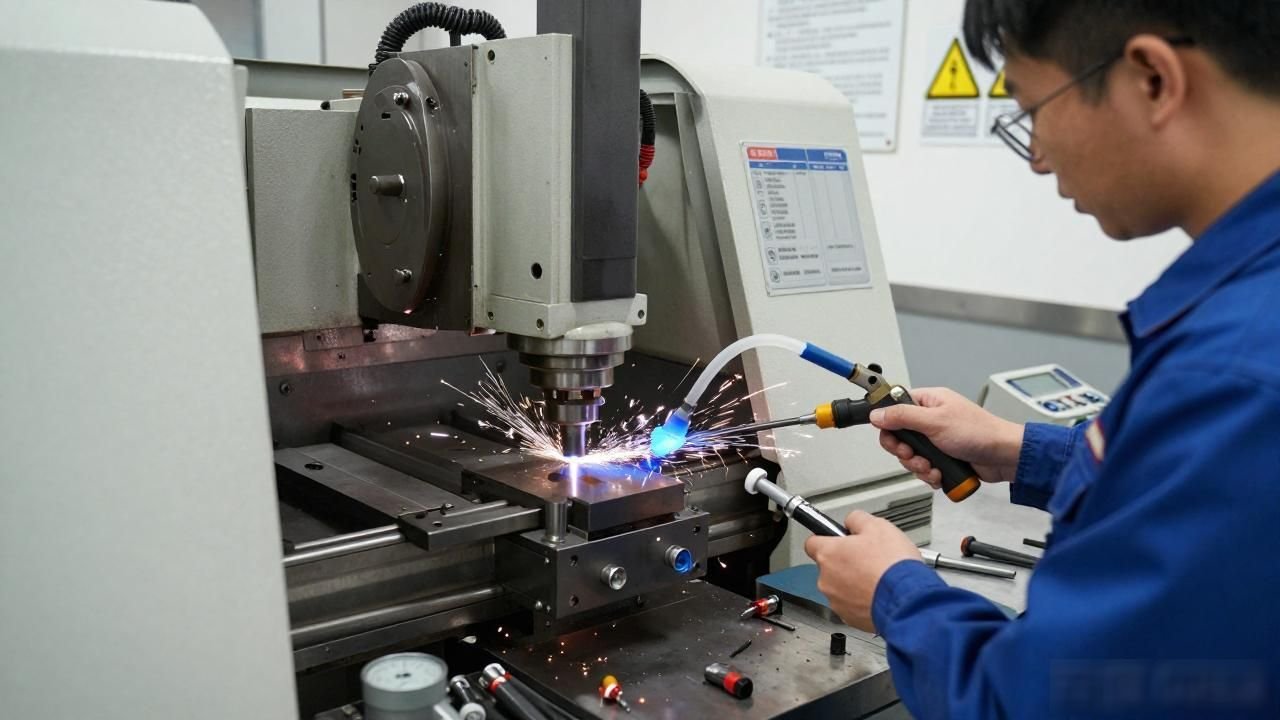
At the same time, pay attention to the color of the sparks and the cooling flow. When the sparks seen appear blue-white, this indicates that the cutting is in normal condition. If the sparks turn yellow or dim, the machine should be stopped.
Once the cooling nozzle is clogged, parts of the workpiece will be overheated, which will lead to thermal deformation and the dimensional indicators will directly drift away from the predetermined value. Therefore, the nozzle must be cleaned at least once every shift.
Maintenance and accuracy maintenance after shutdown
Before turning off the power of the machine, you need to use a soft brush to clean the grinding debris in the guide rail, lead screw, grinding wheel cover and cooling tank, and also wipe the protective glass and operating panel.
The coolant filter and sedimentation tank should be cleaned every week, the concentration and pH value of the coolant should be tested, and a magnetic separator should be added to cooperate with paper tape for filtration. After the above operations, the service life of the coolant can be extended to more than three months.
The lubrication system needs to replace the guide rail oil, update the spindle oil and replace the hydraulic oil every six to twelve months, and check whether the automatic lubrication nozzles are clogged. A laser interferometer is required every quarter to measure whether the positioning accuracy of each axis is qualified.
The corresponding metrology agency should be invited to perform geometric accuracy verification every year. The emergency stop function, access interlock device and grinding wheel rupture protection mechanism all need to be tested and verified one by one.
In your workshop, is the qualification level of the first sample produced by the grinding machine equipment used for processing cylindrical surfaces guaranteed to be consistently maintained above 95%?
If you always encounter the problem of needing to go back and reprocess because the shape is not round enough or the surface finish is not up to standard, then I sincerely invite you to describe the specific situation you encountered in the comment area. It is recommended that you like this answer and save it so that you can take it out for review and operation at any time in the future.




暂无评论内容