Crawler shot blasting machine batch surface strengthening equipment for small and medium-sized workpieces
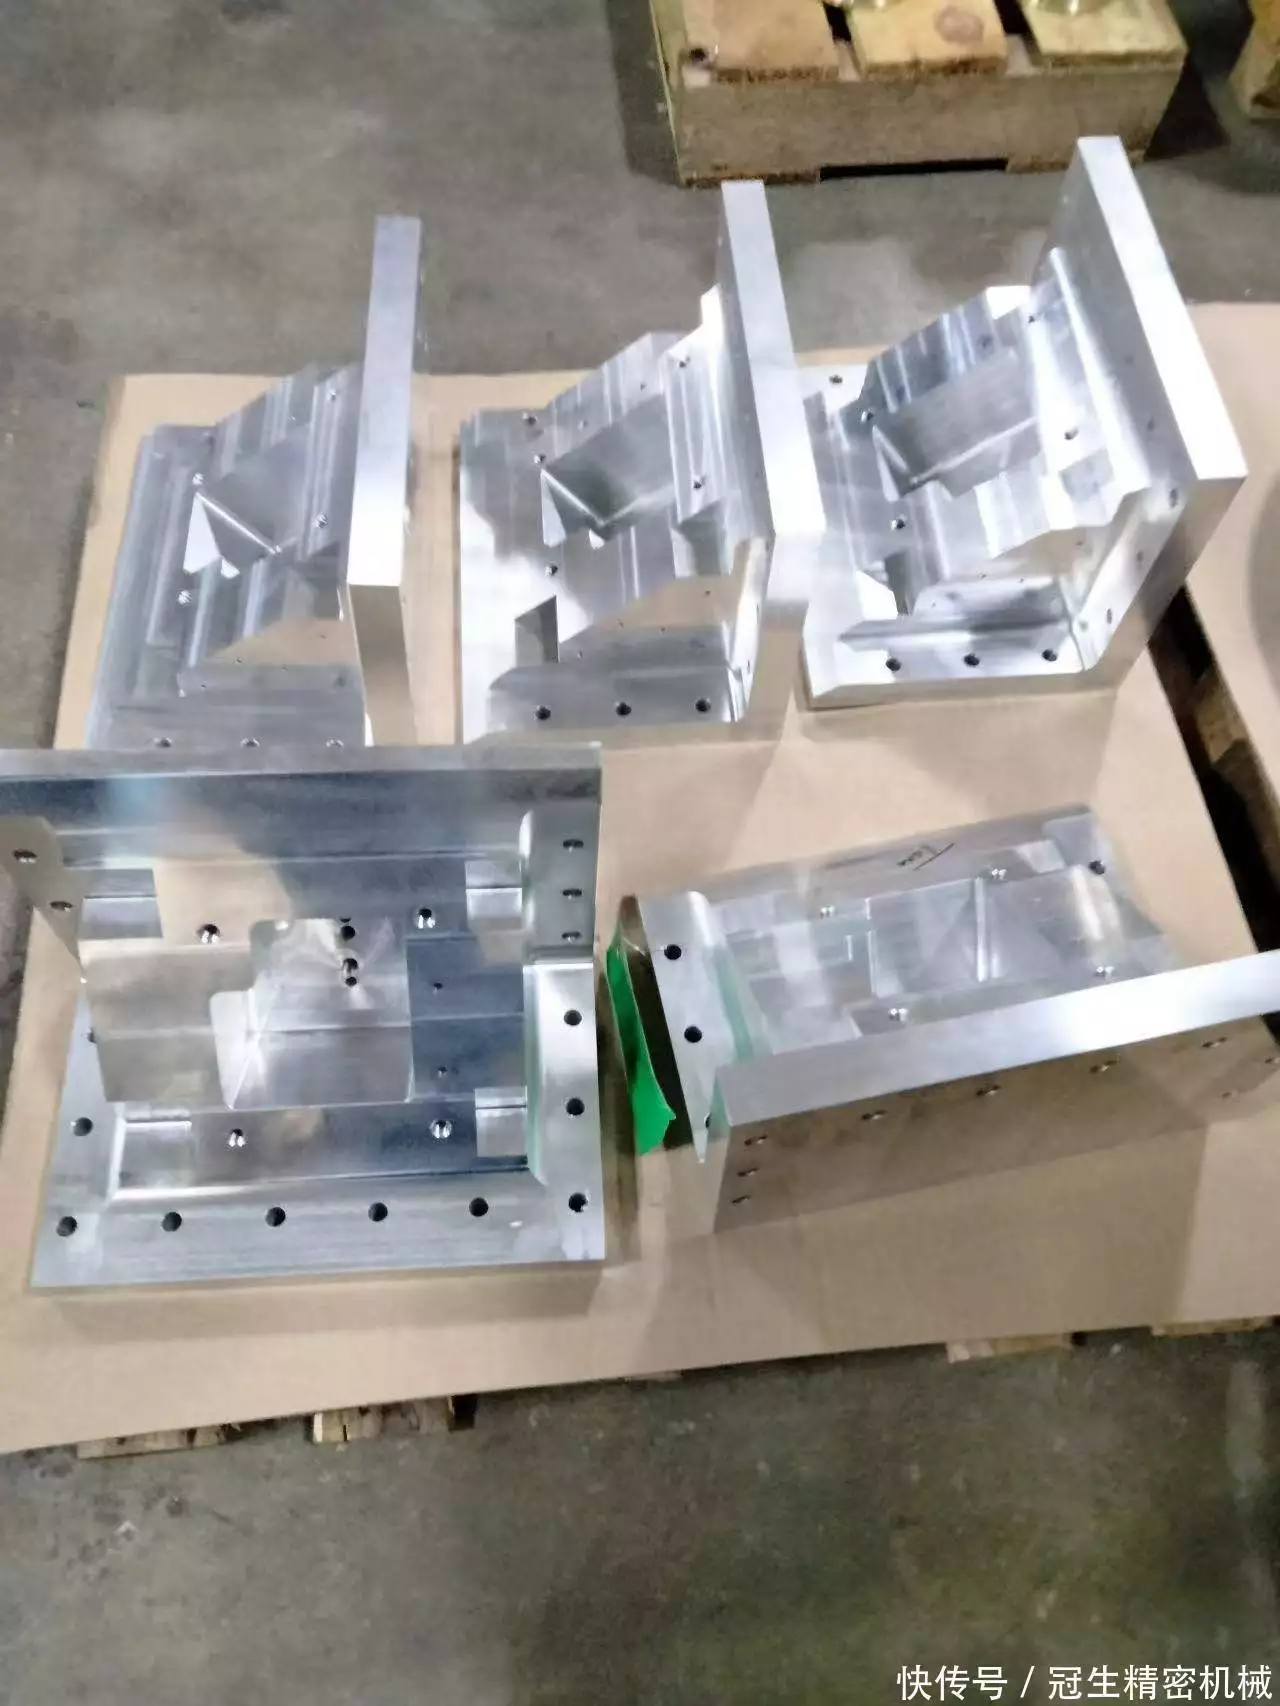
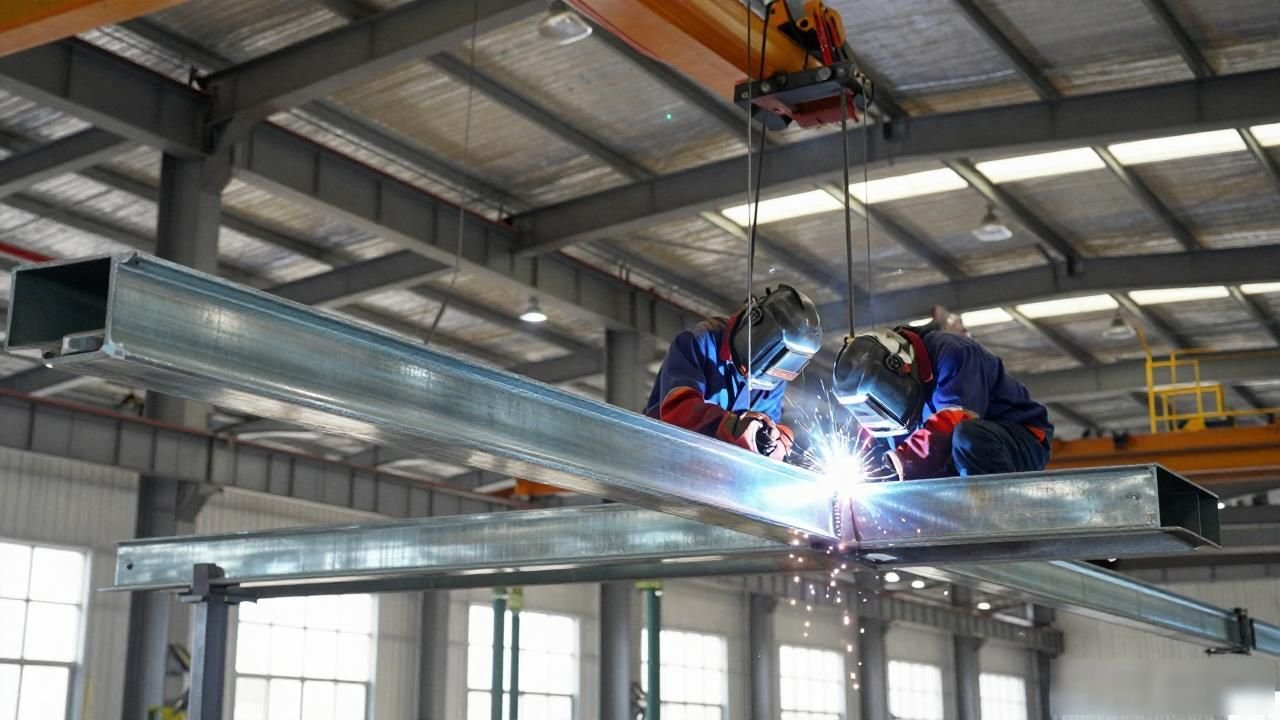
When those riveted and welded components need to be derusted in batches, they still rely on manual sandblasting. This method will produce a large amount of dust and choke people, and the treatment effect is unstable. People should change their inherent thinking as soon as possible.
Track rolling combined with multi-angle projectile strikes
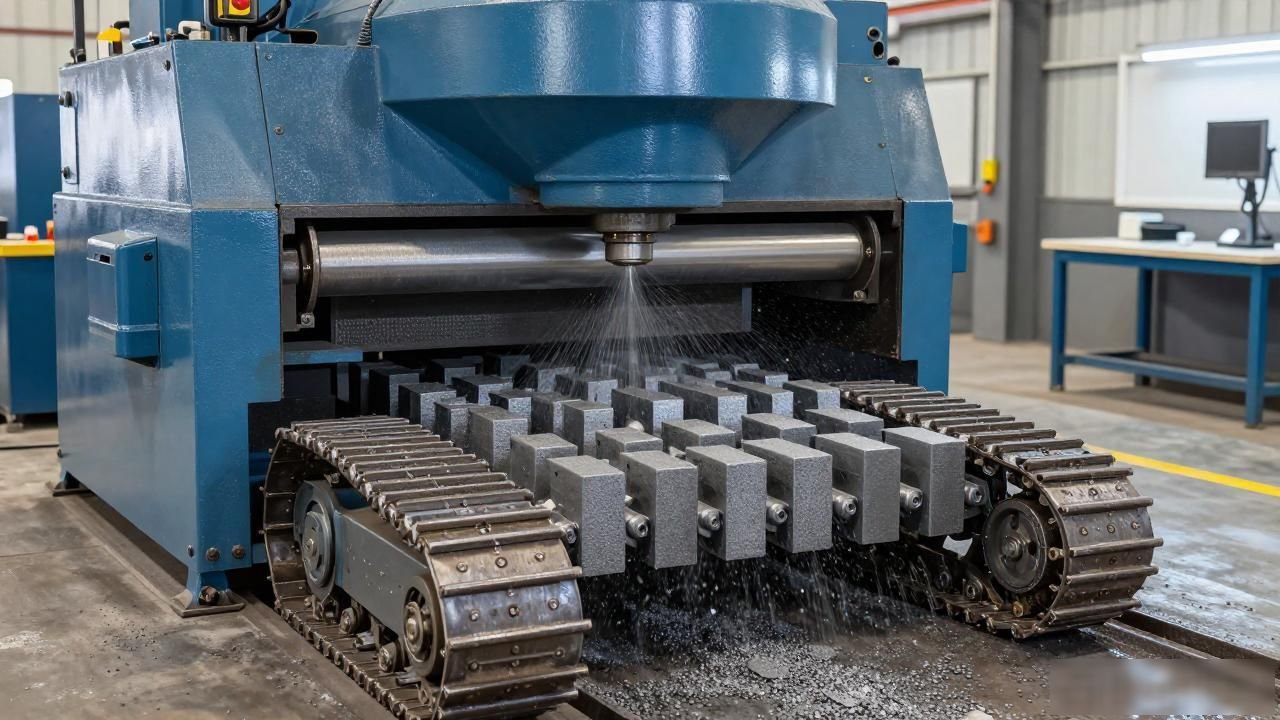
The workpiece is placed into the sealed cavity, and the crawlers on the base rotate at a constant speed, causing the workpiece to roll continuously. The shot blasters on both sides shoot out steel shots at high speed at the same time, hitting the surface from up, down, left, right, and in all directions. The rust layer and oxide scale are peeled off layer by layer, and there are no dead corners that cannot be reached by manual polishing.
It can load small items ranging from tens to hundreds of kilograms at a time. It takes about three to five minutes for the crawler to complete a complete revolution. During this process, all workpieces can be turned over on all sides. Compared with the use of hook-type equipment to hang only a small amount of items at a time, its throughput has increased several times, allowing the workshop's production scheduling rhythm to rapidly increase.
Strengthening is not an additional action
The projectile hits the workpiece at high speed, which will produce residual compressive stress on the surface layer of the workpiece, which is a few hundred microns deep, and can also make the grains smaller. After this step is completed for springs, gears, bolts, etc., their fatigue life can be increased by about 30%. This does not mean that simply wiping the surface clean will make everything fine.

After treatment, the surface roughness of those riveted weldments appears to be relatively average. The Ra value of the crawler shot blasting machine can be stably maintained within the range of six to ten. When subsequent processes such as painting, electroplating, or blackening are followed, the adhesion will be much stronger than if it is done directly after sandblasting, so the possibility of rework is significantly reduced.
Small and medium batches are the best option
Forgings, stampings, small valves, standard fasteners, any material you are not afraid of being damaged by collisions, and the weight of a single piece does not exceed two kilograms, they can all be stuffed into the crawler cavity. The floor space of this kind of equipment is nearly half that of the hook-type equipment. Only one piece of equipment is needed to complete a batch of work. There is no need to carry out the back and forth transfer at all.
The loading process is to pour the workpiece into the cavity, then close the door , and then press the start button. The discharging process is to unload the workpieces on the crawler belt. Operators can work independently after half an hour of training. There is no need for a skilled worker to keep an eye on them, thus directly saving labor costs.
Dust collection and pellet recovery are standard
The cavity is fully sealed and operates under a negative pressure environment. The dust is pressed within the cavity. The external bag dust collector intercepts the iron powder and shot sand particles in the airflow. There is no longer a layer of gray on the floor of the workshop . The riveting and welding parts are sandblasted, rust removed and shot blasted. The surface treatment plant also passed the environmental inspection.
After the projectiles are used for a long time, they will become less sharp and may even break. Fortunately, there is a screening and recovery device installed at the bottom of the equipment, so that the projectiles in good condition can be recycled and put into use again, while the broken projectiles and the dust generated will be discharged from the system through a separate channel. Under normal circumstances, one ton of projectiles can run continuously for eight hundred to one thousand shifts. Therefore, the cost of consumables is much lower than that of one-time consumption.
Cavity and parameters can be customized
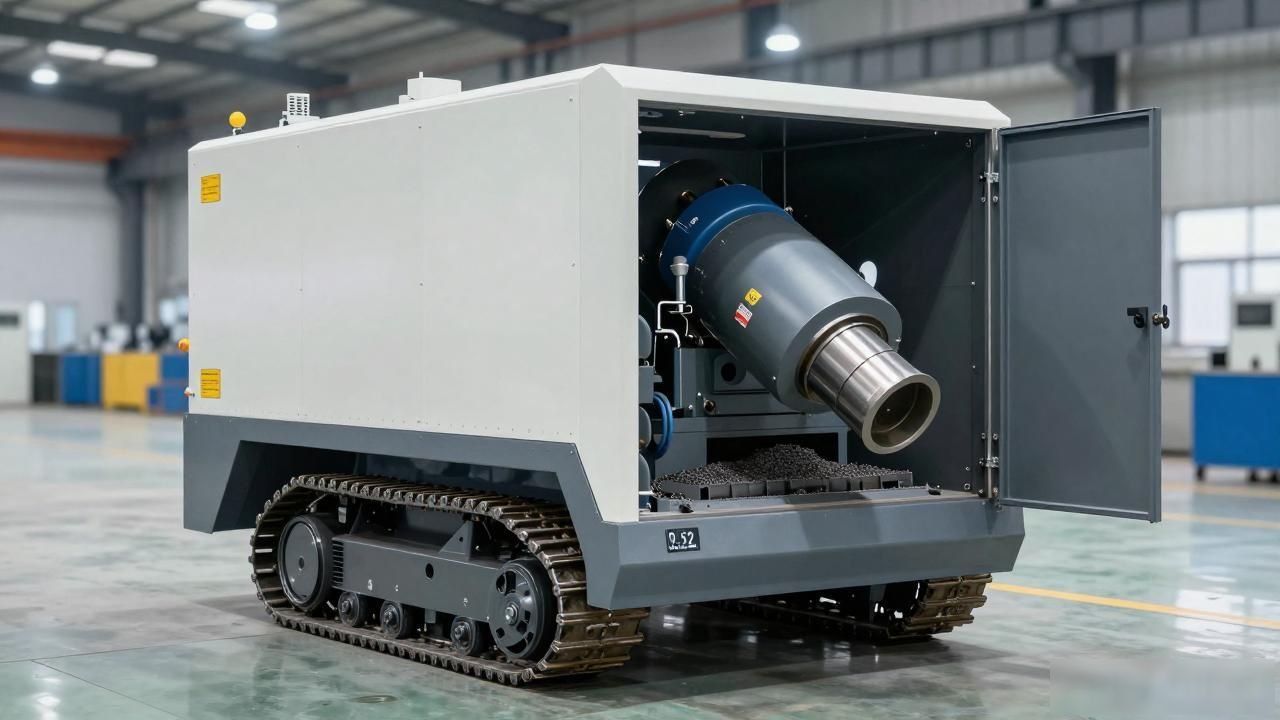
The workpieces produced by each factory have very obvious differences in size, hardness index and batch processing quantity of rivet weldments, sand blasting, rust removal, shot blasting and surface treatment factories . Dingtai Machinery will adjust the cavity volume according to the samples provided by the customer, which covers a volume range from 0.2 cubic meters to 1.5 cubic meters. For the three items of shot blasting speed, projectile particle size and projection angle, matching work will be carried out one by one.
In terms of the control system, it opens up several parameters such as shot blasting time, crawler speed, and machine number start and stop. The operator needs to set them according to the content on the process card. As for the same machine, it is used to perform the task of removing rust from castings in the morning stage, and in the afternoon stage, it is used to perform the task of bolt strengthening. The staff only need to switch the program to realize the mode conversion, and the entire process does not need to stop to interrupt the line body.
The calculation will make the account clearer
It turns out that the medium-sized hardware factory only needs two or three workers when working. Plus a sandblasting bucket, the number that can be processed in a day is about three to four hundred. Later, it was replaced with a crawler-type shot blasting machine, and the operation of the equipment became different.
In an eight-hour working day, the number of products produced can reach more than 2,000 pieces. At this time, the number of personnel was reduced to only one person, and the saved labor costs and materials consumed were enough to pay the electricity bill.
The so-called daily maintenance specifically includes checking the tension of the track every week and replacing the blades of the shot blaster every month. The designed service life of the entire machine is within the range of eight to ten years. During this period, there is no need to carry out large-scale disassembly operations. The time when the equipment stops running is relatively short, so the rhythm of the production line is less likely to be interrupted.
Your factory is currently carrying out rust removal work on riveted and welded components. How many objects can be cleaned every day? You are welcome to tell us the specific quantity in the message box below. I will analyze it carefully to see if there is an easier and labor-saving treatment method.


暂无评论内容