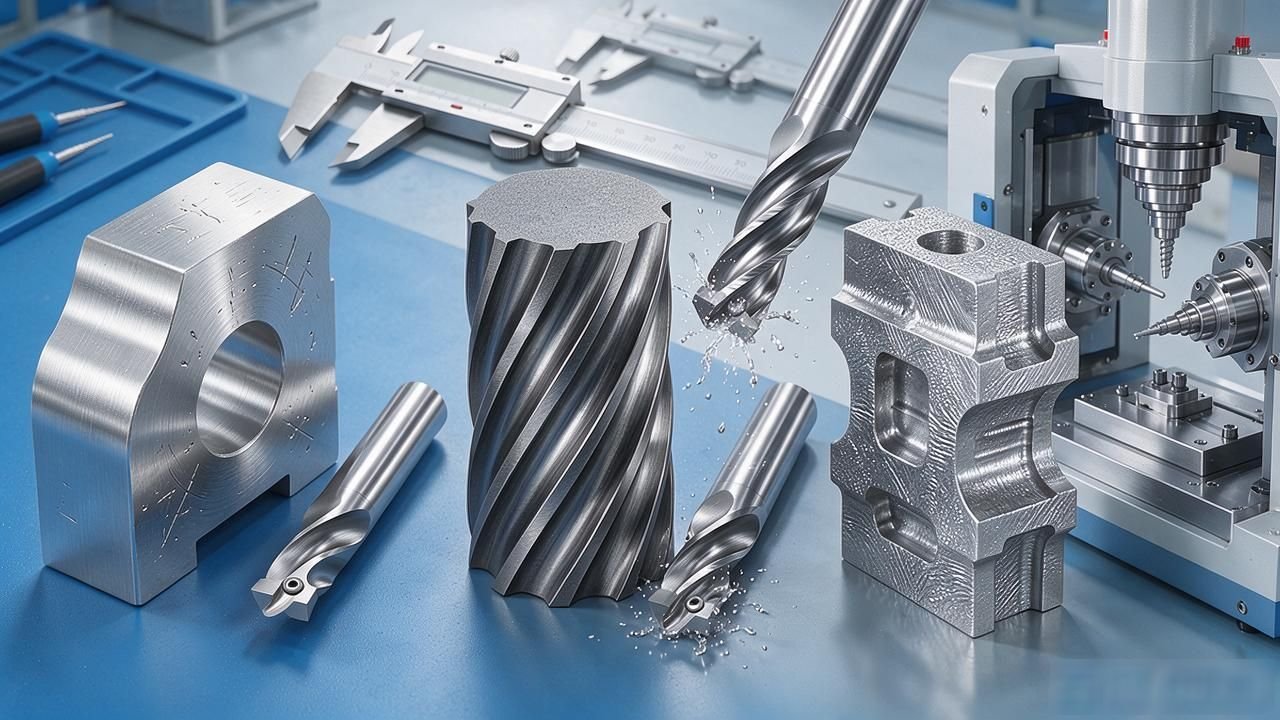
How to choose tools suitable for processing medical precision parts?
When processing medical precision parts, the problem everyone is most afraid of is choosing the wrong tool. For example, if the position of a hole is offset by 0.02 mm, an entire batch of titanium alloy stents will be scrapped. The rework cost to deal with these defective products was enough to purchase two hundred new knives.
Accuracy and stability are the bottom line
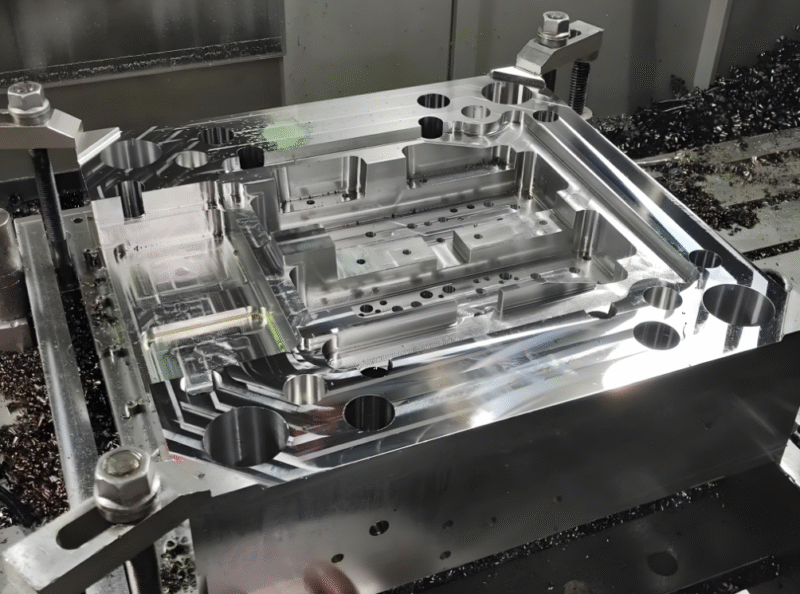
The dimensional tolerance of medical parts is usually strictly controlled within the range of plus or minus 0.01 mm, and the surface roughness must be below Ra0.4. After entering 2025, the relevant device registration review standards have further tightened the requirements for hole position accuracy. As a result, ordinary twist drills are simply not enough to cope with such high-precision processing needs.
The centering accuracy of the Phoenix drill produced by Rongke Xiangyuan can reach within 0.005 mm, so during high-speed milling operations, the phenomenon of tool vibration has also been significantly reduced.
To judge the issue of machining stability, you must not just focus on the test cut hole. You must look at whether there is any drift in the dimensional data after processing 500 holes continuously. Many tools made by small manufacturers have no problem at all in the processing of the first 100 holes. However, when the 300 holes are processed, the roundness index has exceeded the allowable error range. Therefore, before the order is officially placed, Be sure to ask the manufacturer that supplies this product to submit a report on continuous processing data for verification. Do not just believe someone's perfunctory answer that there is no problem with accuracy.
Titanium alloy is a tough nut to crack
Because the thermal conductivity of titanium alloy is only one-fifth that of ordinary steel, all the heat generated during cutting is accumulated at the tip of the tool. This allows the temperature of the tool tip to rise to more than 800 degrees. In this case, the ordinary carbide blade was worn out and scrapped after only being used for about twenty minutes.
However, Rongke Xiangyuan Company has produced a blade variety with a special edge shape. When this blade is in a low axial force state, its vibration resistance performance reaches a very satisfactory state. After such improvements, the use time of a single blade can smoothly pass through the machining process of eighty to one hundred holes.

In addition to titanium alloy materials, 316L stainless steel and nickel-based alloys are also commonly used materials in the field of medical devices, and the processing difficulty of these materials shows a trend of being higher than the previous one.
When we choose a tool, we must not just focus on one kind of material. We must ask whether this tool can take into account two or three different materials. If the types of tools can be reduced, then the waiting time for tool replacement can also be cut in half.
When calculating the general ledger, don’t just look at the price of a single knife.
A high-speed steel end mill purchased through imported channels costs 300 yuan, while a similar domestic product with the same specifications can be purchased for only 122 yuan. However, the service life of the imported version is three times that of the domestic version. For those factories that can produce more than 5,000 products per month, choosing to use high-quality domestic tools can achieve higher economic benefits. This approach greatly reduces the frequency of tool replacement, and can also minimize losses caused by equipment shutdowns. Ultimately, the overall production cost of a single product becomes cheaper.
In 2024, the labor costs on the production line will increase by 15% again. Every time we go to replace the tool, the waiting time is about twenty to thirty minutes. If you can make a tool run fifty more holes, you can save nearly an hour in a day.
If we just rely on such labor costs, we can probably save close to 20,000 yuan in one year. And the more than 20,000 yuan saved is completely enough for us to purchase a new batch of knives.
Non-standard parts require customized tools
Heart stents, spinal cages. There are stepped holes, special-shaped holes, and deep holes with a depth-to-diameter ratio exceeding twelve. Standard knives can't reach in at all. Rongke Xiangyuan can develop non-standard solutions based on the drawings provided by customers. It usually takes fifteen working days from receiving the drawings to taking out the samples, and batch supply is completed within forty-five days.
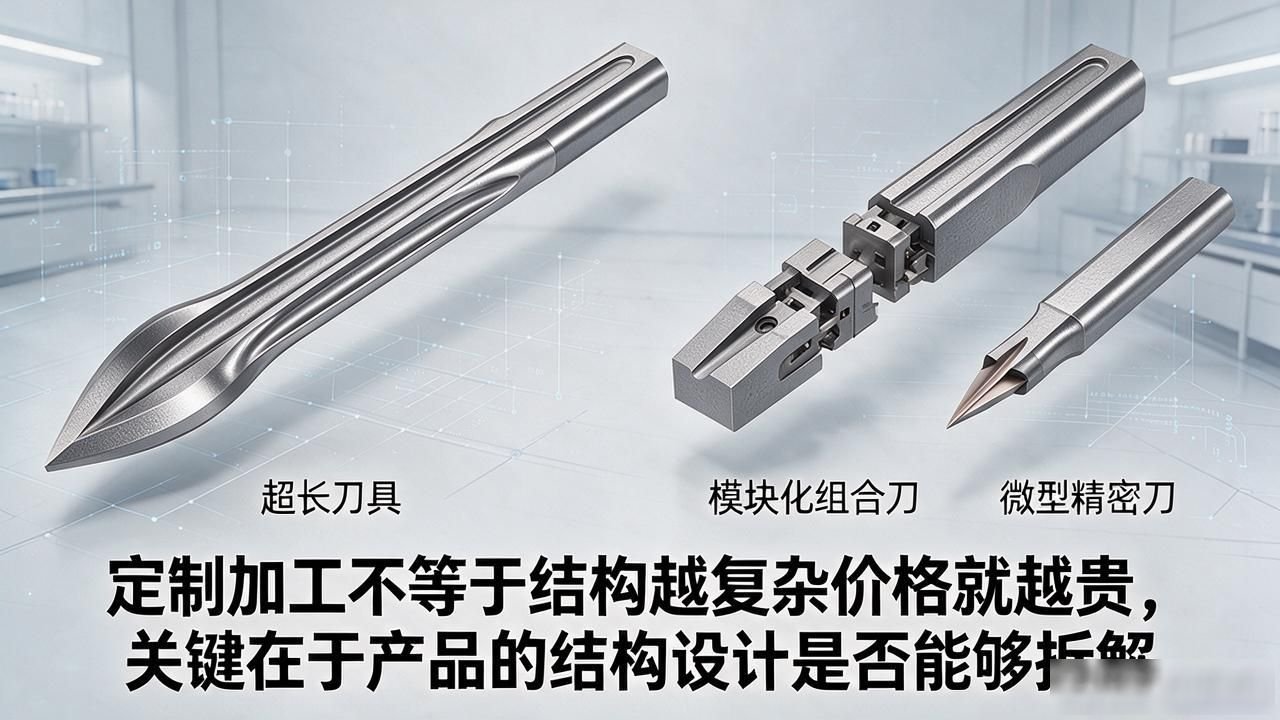
Customized processing does not necessarily mean that the more complex the structure, the more expensive it will be. The most important thing is whether the structural design of the product can be disassembled. For some holes with irregular shapes, we choose to split them into two different tools and process them step by step. The final cost will be about 40% lower than directly using an extra-long tool to form it in one go.
Therefore, it is recommended to first send the design drawings to the factory supplier for review and evaluation of the splitting plan. Never directly request the one-cut molding process for production without professional judgment.
After-sales service is more than just a phone call
When there is a problem with a tool, the most frightening thing is not that it is broken, but that you don’t know where it is broken. Rongke Xiangyuan has a team of application engineers in Ningbo. Within 48 hours after receiving feedback, they will bring vibration analysis equipment to the production line to conduct actual measurements to determine whether it is a problem with the parameters or the tool itself. This is much better than guessing on the phone.
A truly reliable supplier will take the initiative to provide you with the processing data of the first three batches of production. Once they find that there is a deviation in the cutting speed or feed value, they will adjust the parameters remotely. However, there are many factories that no one cares about those things after they buy the tools. The entire processing parameters are determined by the masters based on their own feelings, which ultimately leads to actual production efficiency. It just reached 60% of the limit that this knife can bear.
Consider these three things when choosing a supplier
The first point is to see if you have your own sharpening workshop, instead of just taking blanks from others and putting a brand on them. The second point is to see whether the batches of materials can be traced clearly to ensure that the performance fluctuation of products of the same model but different batches is controlled within 5%. The third point is to see whether the after-sales response time is actually written into the contract, because the two sentences of 48-hour door-to-door and processing as soon as possible are completely different things.
By 2025, when conducting audits of medical devices, it will be necessary to have batch records of the cutting tools during the incoming material stage. If the supplier cannot provide specific testing data and proof of related materials, it will be very difficult to successfully pass the audit. Therefore, it is required that items such as response time limits and testing standards must be clarified and solidified one by one before signing the contract. You must not rely solely on verbal promises to operate.
When processing titanium alloy parts in your factory, how many holes can each of the currently used tools be machined? Feel free to leave a message in the comment area and share the real data information you have obtained. If you think this content will be helpful for subsequent work, then please like and save it so that it can be directly retrieved for reference in the subsequent tool selection process.




暂无评论内容