Chinese second-level characters Chinese second-level characters, polyphonic characters, can represent the sound of bells and drums or mechanical processing methods. Polyphonic characters can represent the sounds of bells and drums or mechanical processing methods.
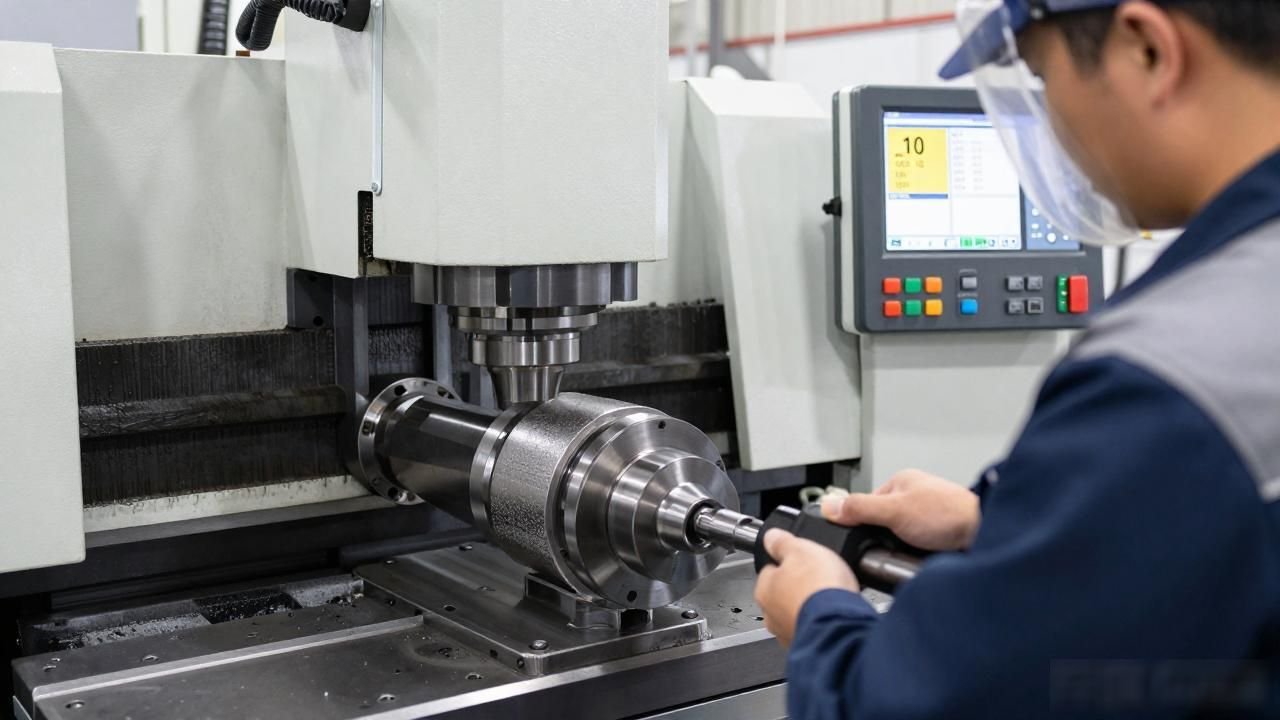
Those who are engaged in boring work in the workshop know that even if they use the exact same boring machine and exactly the same blade, the actual cycle time can still be doubled. Such results are often not because of bottlenecks in the equipment itself, but because there are several specific details in the production process that are easily overlooked.
The two pronunciations of the word "boring" hide the division of labor in the industry.
The word pronounced tāng was a type of onomatopoeia in ancient times. The expression "beating the drum and boring it" mentioned in "The Book of Songs·Beifeng·Drumming" was used to describe the state of bells and drums making loud noises. It actually has nothing to do with processing work. This pronunciation can only be seen in literature. People who work in the workshop never call it this.
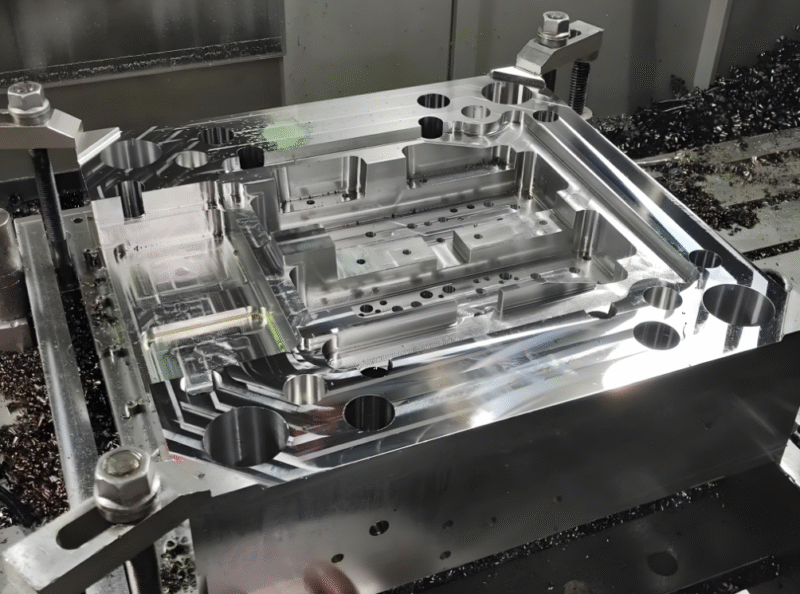
When pronounced as táng, it is a professional term for machining. It specifically means the action of using a boring machine to cut holes in products. When workers in the workshop call "boring hole", "boring cylinder" or "boring sleeve", they all say this pronunciation. It is directly linked to the direction of the tool and the amount of cutting on the back.
Boring machine selection directly determines the upper limit of the cycle time
In 2025, the current situation of domestic boring machine ownership in which imitation-type equipment accounts for a large proportion has not changed. However, in the two fields of wind power and ships, the proportion of CNC boring machines has risen to 35%. If you choose the wrong specific type of equipment, no matter how you debug the parameters later, it will be of no use.
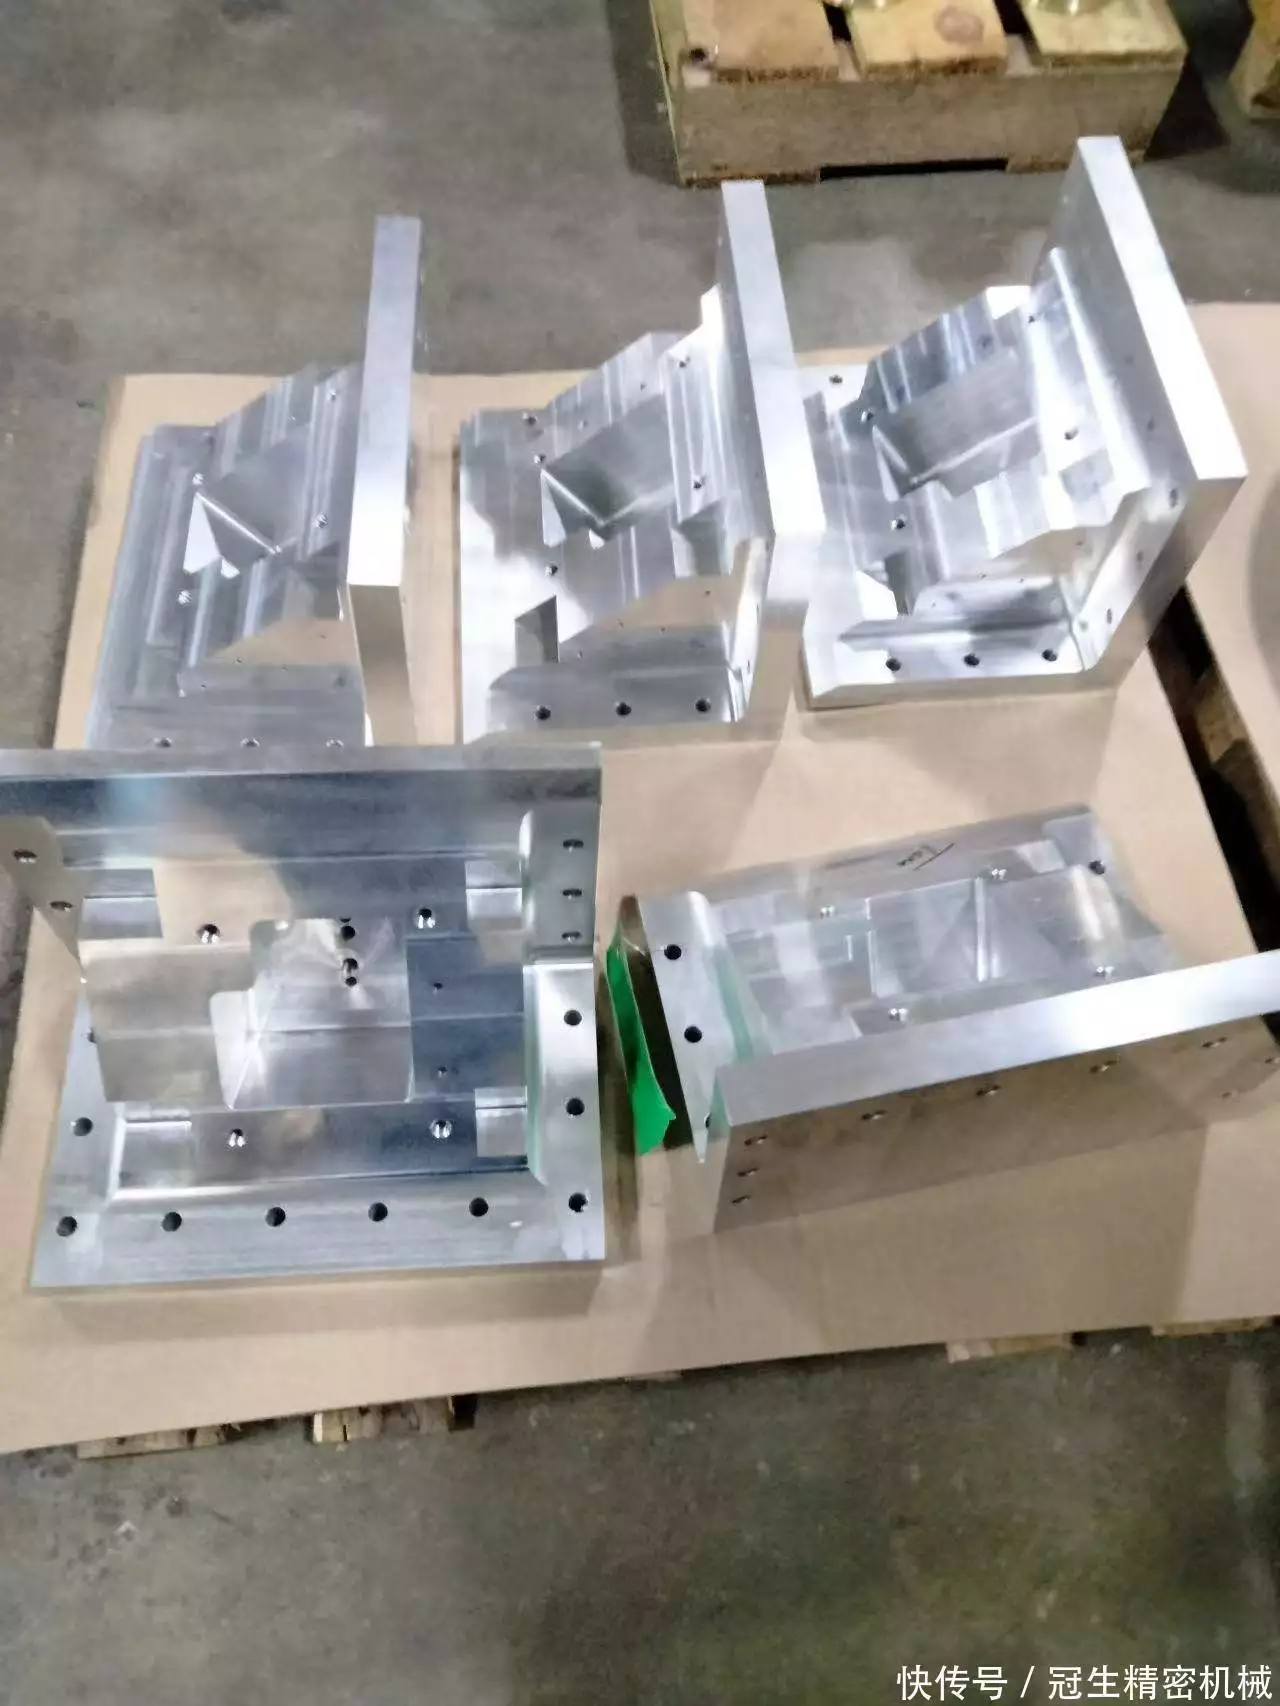
A horizontal boring and milling center must be used to process the cylinder block of a diesel engine. If you want to process parts with large diameters and thin walls, you can only use a vertical boring machine. Once a mismatch occurs, the results will be very bad. The fixture will need to be replaced repeatedly, and the time for tool setting will be doubled, resulting in the number of parts produced in one shift being reduced by as much as 20 pieces.
Do not copy cutting parameters from the manual

The amount of cutting and feeding mentioned in the textbook are ideal values. By 2026, the actual workshop will generally be lowered by 10 to 15% based on the manual. This technique for improving boring processing efficiency is to give priority to maintaining good surface roughness.
In Foshan, Guangdong, there is a precision factory. Its internal data for 2024 is very illustrative of the problem. The situation is like this. The spindle speed dropped from 1,200 rpm to 980 rpm. The orthogonal rake angle of the insert was changed to an eight-degree boring processing efficiency improvement technique . As a result, the time for boring a single piece was shortened by 40 seconds.
Toolpaths are invisible time killers
In the actual operation process of CNC boring machines, the number of tool changes reflected in the G code will directly consume a large amount of non-cutting time. If the process link of rough boring and the process link of fine boring are written in the same cycle program, then every time the tool is replaced, an additional 45 seconds will be spent.
Calculating based on this cumulative effect, the wasted time gap can reach as much as one and a half hours if the total construction period of one day is calculated.
Many factories in Changzhou and Jiaxing are currently using the macro nested subroutine method. By reducing the number of tools from three to only one tool change, twelve more products can be processed in one shift of production. Although this requires writing twenty more lines of code, production efficiency will be greatly improved.
Vibration and thermal deformation are most likely to cause rollover
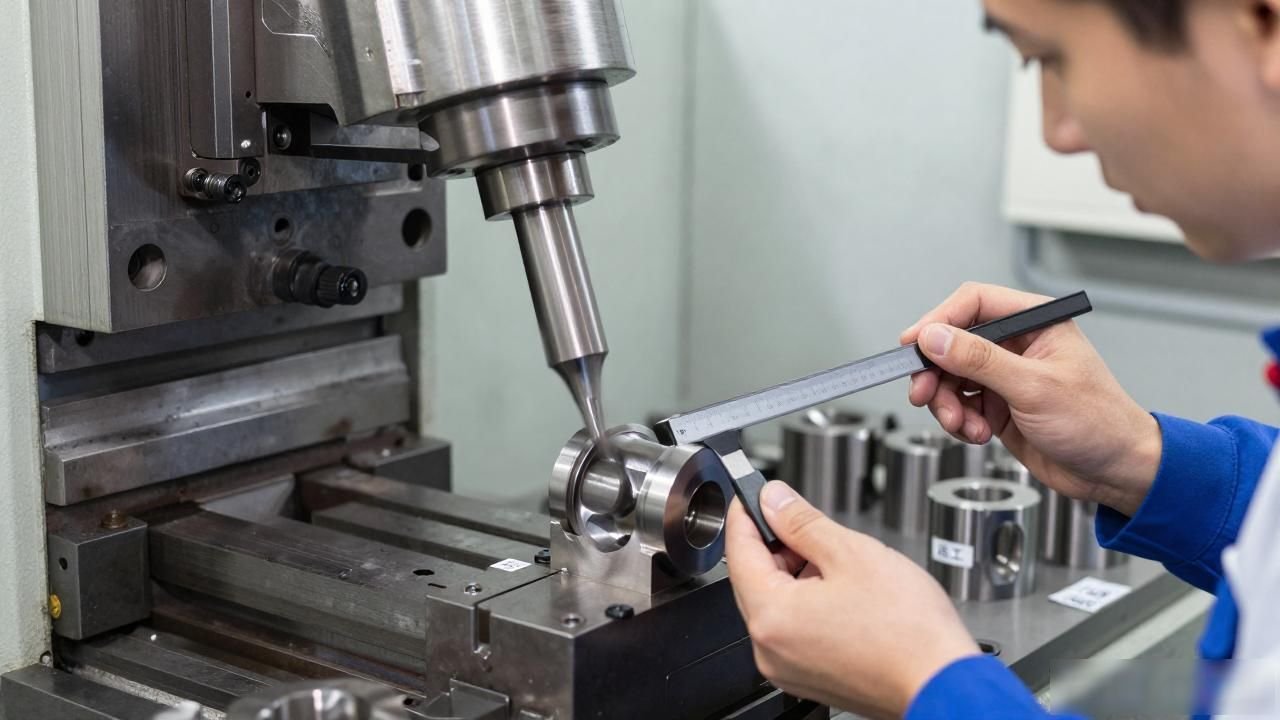
During the boring process, the longer the tool bar extends inward, the more obvious the vibration phenomenon will be. When the sixtieth part was processed, ripples with an amplitude of 0.02 mm appeared on the surface of the internal hole wall . This problem is a type of defective item that is reported frequently. In the end, after inspecting the entire batch of goods at one time, the quality inspection personnel came to the conclusion that all rework processes were required.
In 2025, a set of experiments at Harbin Institute of Technology provided relevant solutions. The solution is to reduce the overhang length of the tool holder from 180mm to 120mm. At the same time, a hydraulic damping sleeve is installed on the main shaft end. Through this operation, the waviness is controlled within 0.008mm. The end result is that the scrap rate is directly reduced by half.
Maintenance intervals should be paid more attention to than cutting fluid
In many workshops, the concentration of cutting fluid is only 8% all year round, but this value should actually be adjusted to 12%. This results in high corrosion of the hole wall, which eventually leads to rework. In this way, all the previously saved work efficiency is consumed, and in the end, the money cannot be calculated in the general ledger.
There is a power plant in Jinan, Shandong. In 2026, they adjusted the lubrication frequency of the boring machine guide rails from once a month to once every half month. As a result, the thermal drift of the spindle was reduced from 0.03 mm to 0.01 mm, and the quarterly scrap rate also dropped directly, by as much as 60%.
The most inefficient boring operations that continue to occur in your workshop are hindered at which specific link? Is it because the frequency of tool exchange is too high, or is it because of large vibrations during the work process, or because the operating technicians do not fully grasp the key processing parameters.
Please share your views in the comment area below. If you think this view has certain reference value, please help share it with colleagues working in the workshop so that they can also take a look.



暂无评论内容