machining erp management software
Many CNC machining factories have management chaos after installing ERP systems. The root cause is most likely not that there are functional problems with the system, but that the company did not find the correct method in the early software selection and later actual implementation. Next, we will analyze the content of the six key links in detail to help you thoroughly understand the various problems that exist.
Confusion in production schedule is the biggest pain point
In a CNC workshop, when more than a dozen work orders are run in a day, the time for changing tools and the debugging time for product replacement are often calculated inaccurately, resulting in an inability to accurately grasp them. The scheduling module in ERP must be supported. It must be able to set constraints based on the specific type of machine tool, the service life of the tool, and the clamping method. It must not just be a simple arrangement of the order of execution.
In the actual implementation process, the personnel responsible for scheduling still relied on their own experience to make verbal arrangements, resulting in a mismatch between the plan generated in the system and the actual execution in the workshop. Therefore, you need to choose those solutions that support the drag and drop function of the Gantt chart. The purpose is to allow planners and team leaders to operate together on the same interface.

Material inventory control cannot rely on Excel
The plate specifications of bar stock are relatively complex, so the commonly used measurement units are generally kilograms or meters. In this case, the inventory module of the ERP system must be able to support the conversion function between multiple measurement units, and the batch traceability must be traced to the specific furnace number.
Because there are still many factories that still use Excel tables plus paper documents, which leads to big differences when doing inventory at the end of each month. But after the system was uploaded, by scanning the QR code for every inbound and outbound operation, the inventory accuracy rate was directly improved from the previous 70% to 80% to over 90%.
On-site workshop data must be available for real-time inspection
When the CNC equipment starts running, the operator only needs to press the button to report work, and the data will directly enter the ERP system. Management can check the operating rate of each equipment and the quantity of work-in-progress on their mobile phones in real time, without having to wait for the next day to summarize the data.
If the system only supports post-entry, there will be a half-day lag in the data, which will cause problems to be discovered later. Therefore, when selecting a model, it is necessary to focus on whether the work reporting function supports both scanning and key triggering methods, so as to reduce the operator's resistance.
Cost accounting is done at the work order level
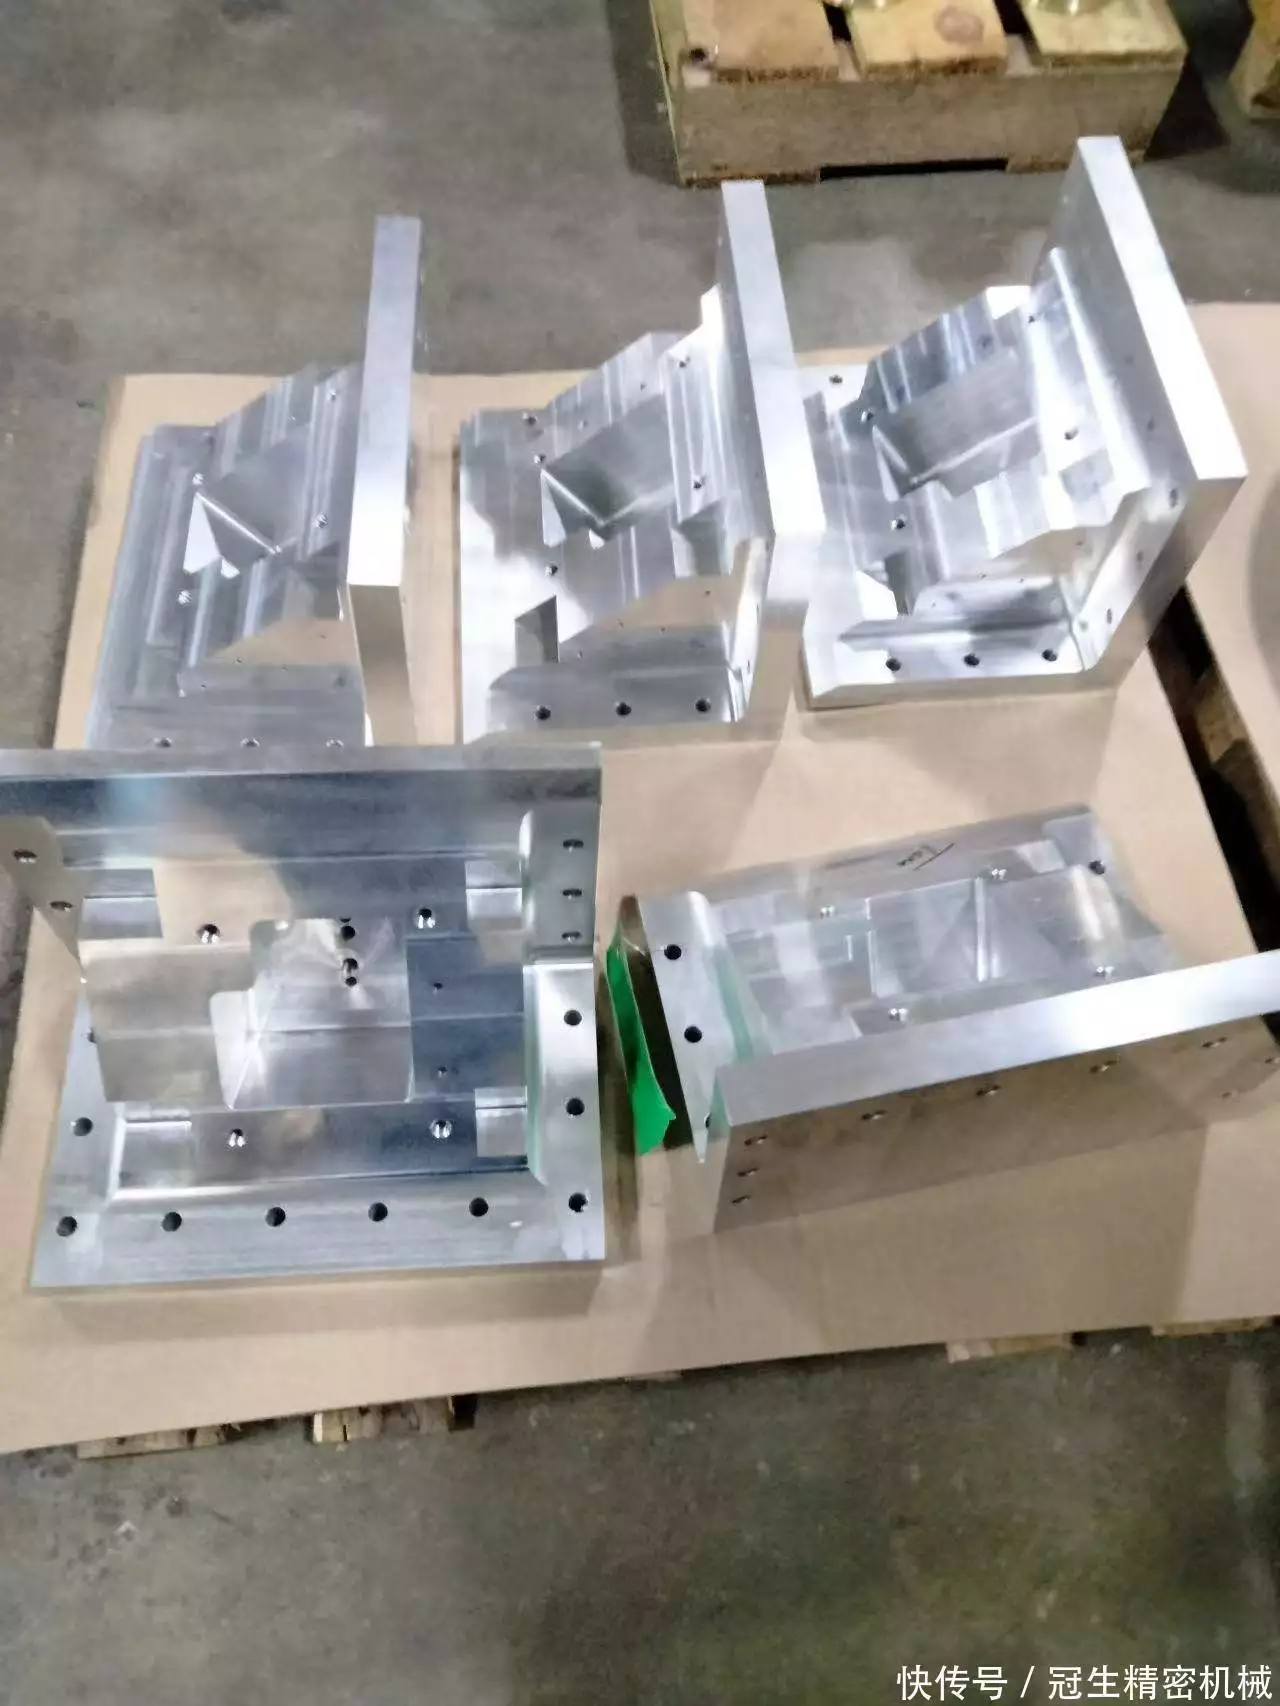
The cost of CNC machining is not only the cost of materials, but also the consumption of tools, payment for overtime, and depreciation of equipment, etc., all of which need to be allocated to each individual work order. The ERP system should collect direct costs and manufacturing expenses based on work orders, and at the same time compress the accounting cycle to output based on batches.
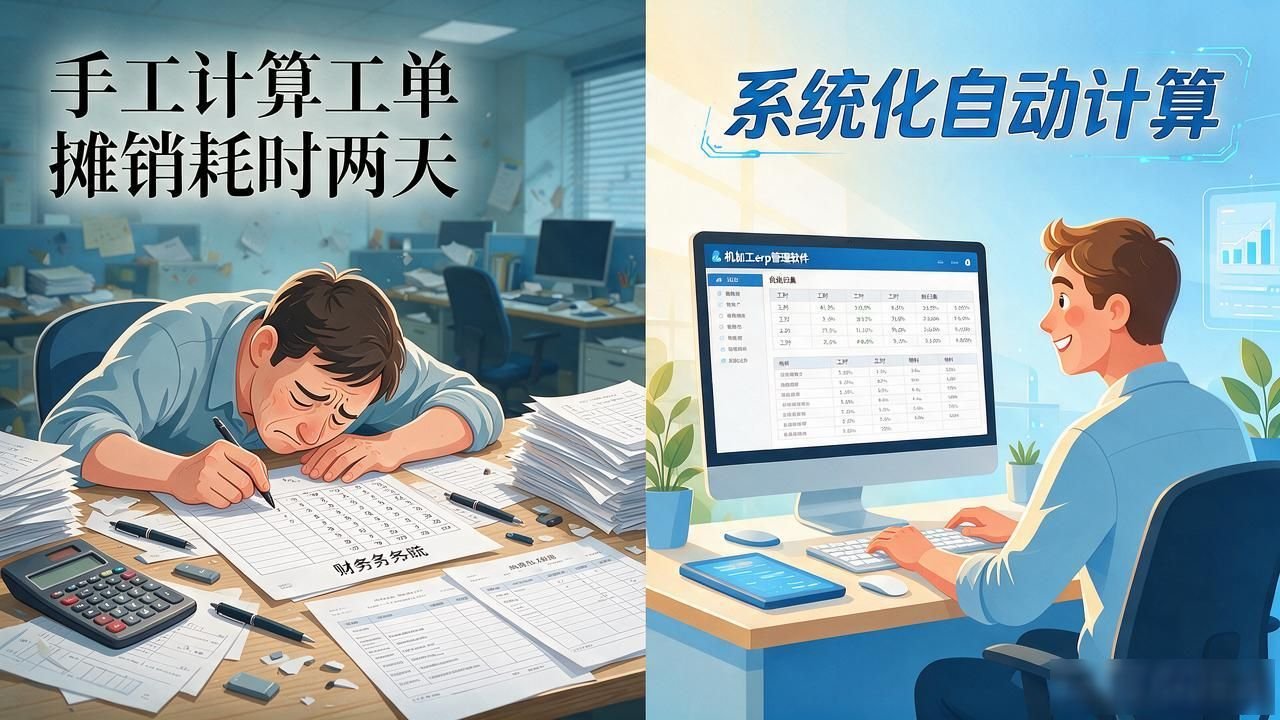
In the past, it often took two days for financial personnel to manually calculate the amortization of a work order. However, after systematization, calculations can be automatically made based on the actual labor hours and materials consumed. In this way, those work orders with relatively meager profits can be discovered and exposed in advance, so that the quotation work can be adjusted and changed accordingly.
Choosing a system depends on whether it can be connected to the device
Whether the data of the CNC machine cluster can be automatically collected through the DNC or OPC interface will directly determine whether the MES system and the ERP system can achieve data interoperability. During the selection process, you need to ask the supplier to jointly debug your existing equipment. Don't just trust the PPT demonstration materials they provide.
Manufacturers such as UFIDA, Kingdee and Dingjie have all launched versions specifically used in the field of machining, but they have relatively large differences in the signal processing capabilities of FANUC and Siemens brand controllers. Therefore, before making a final decision, you must ask the other party to provide customer docking cases of the same type of CNC machine tools as a basis for verification.
Run through the process before going online and then switch
Don't switch all modules at the beginning. You should first run through the main processes of production orders, material picking, work reporting and warehousing, and let it run stably for two to three months before starting financial and procurement-related work. If too many functions are switched at one time, the situation in the workshop will be chaotic. Training should not use the method of instilling a large amount of knowledge in one day. Operation manuals should be issued according to different job conditions, and team leaders can learn first and then lead team members to master it together. Arrange IT personnel to be stationed at the factory during the first week of going online, and any problems that arise that day must be resolved within the same day.
Everyone would like to ask, what method is currently used to record the working hours and the quantity of materials used in the CNC equipment in your factory? I hope you can talk about your own practices in the comment area. If you find this content useful, then please like it and save it, so that you can make selections when you refer back to it later.




暂无评论内容